
How to Source Machined Casting Components Without Scope Gaps
Direct answer
Machined casting components create risk when the casting supplier, machining supplier and buyer each assume someone else owns the final dimensions. A reliable RFQ should define as-cast surfaces, machined surfaces, datum features, machining allowance, tolerance priorities, surface finish, inspection records and final responsibility. The best supplier discussion treats casting and CNC machining as one manufacturing route, not two separate purchases joined at the end.
Sourcing is simpler when one supplier both casts and machines the component. Waking’s CNC machined castings page covers that combined route.
Table of Contents
- Direct answer
- Supplier scorecard
- RFQ evidence checklist
- Common mistakes and risk matrix
- Procurement checklist
- FAQ
Supplier scorecard
| Audit area | What a buyer should verify | How to check it |
|---|---|---|
| As-cast features | Which areas can remain as-cast without affecting function? | Mark non-critical surfaces clearly. |
| Machined features | Which faces, bores, holes, threads or sealing areas need CNC machining? | Show final dimensions and datums. |
| Fixture strategy | Can the rough casting be located repeatably for machining? | Discuss datum surfaces and stock allowance. |
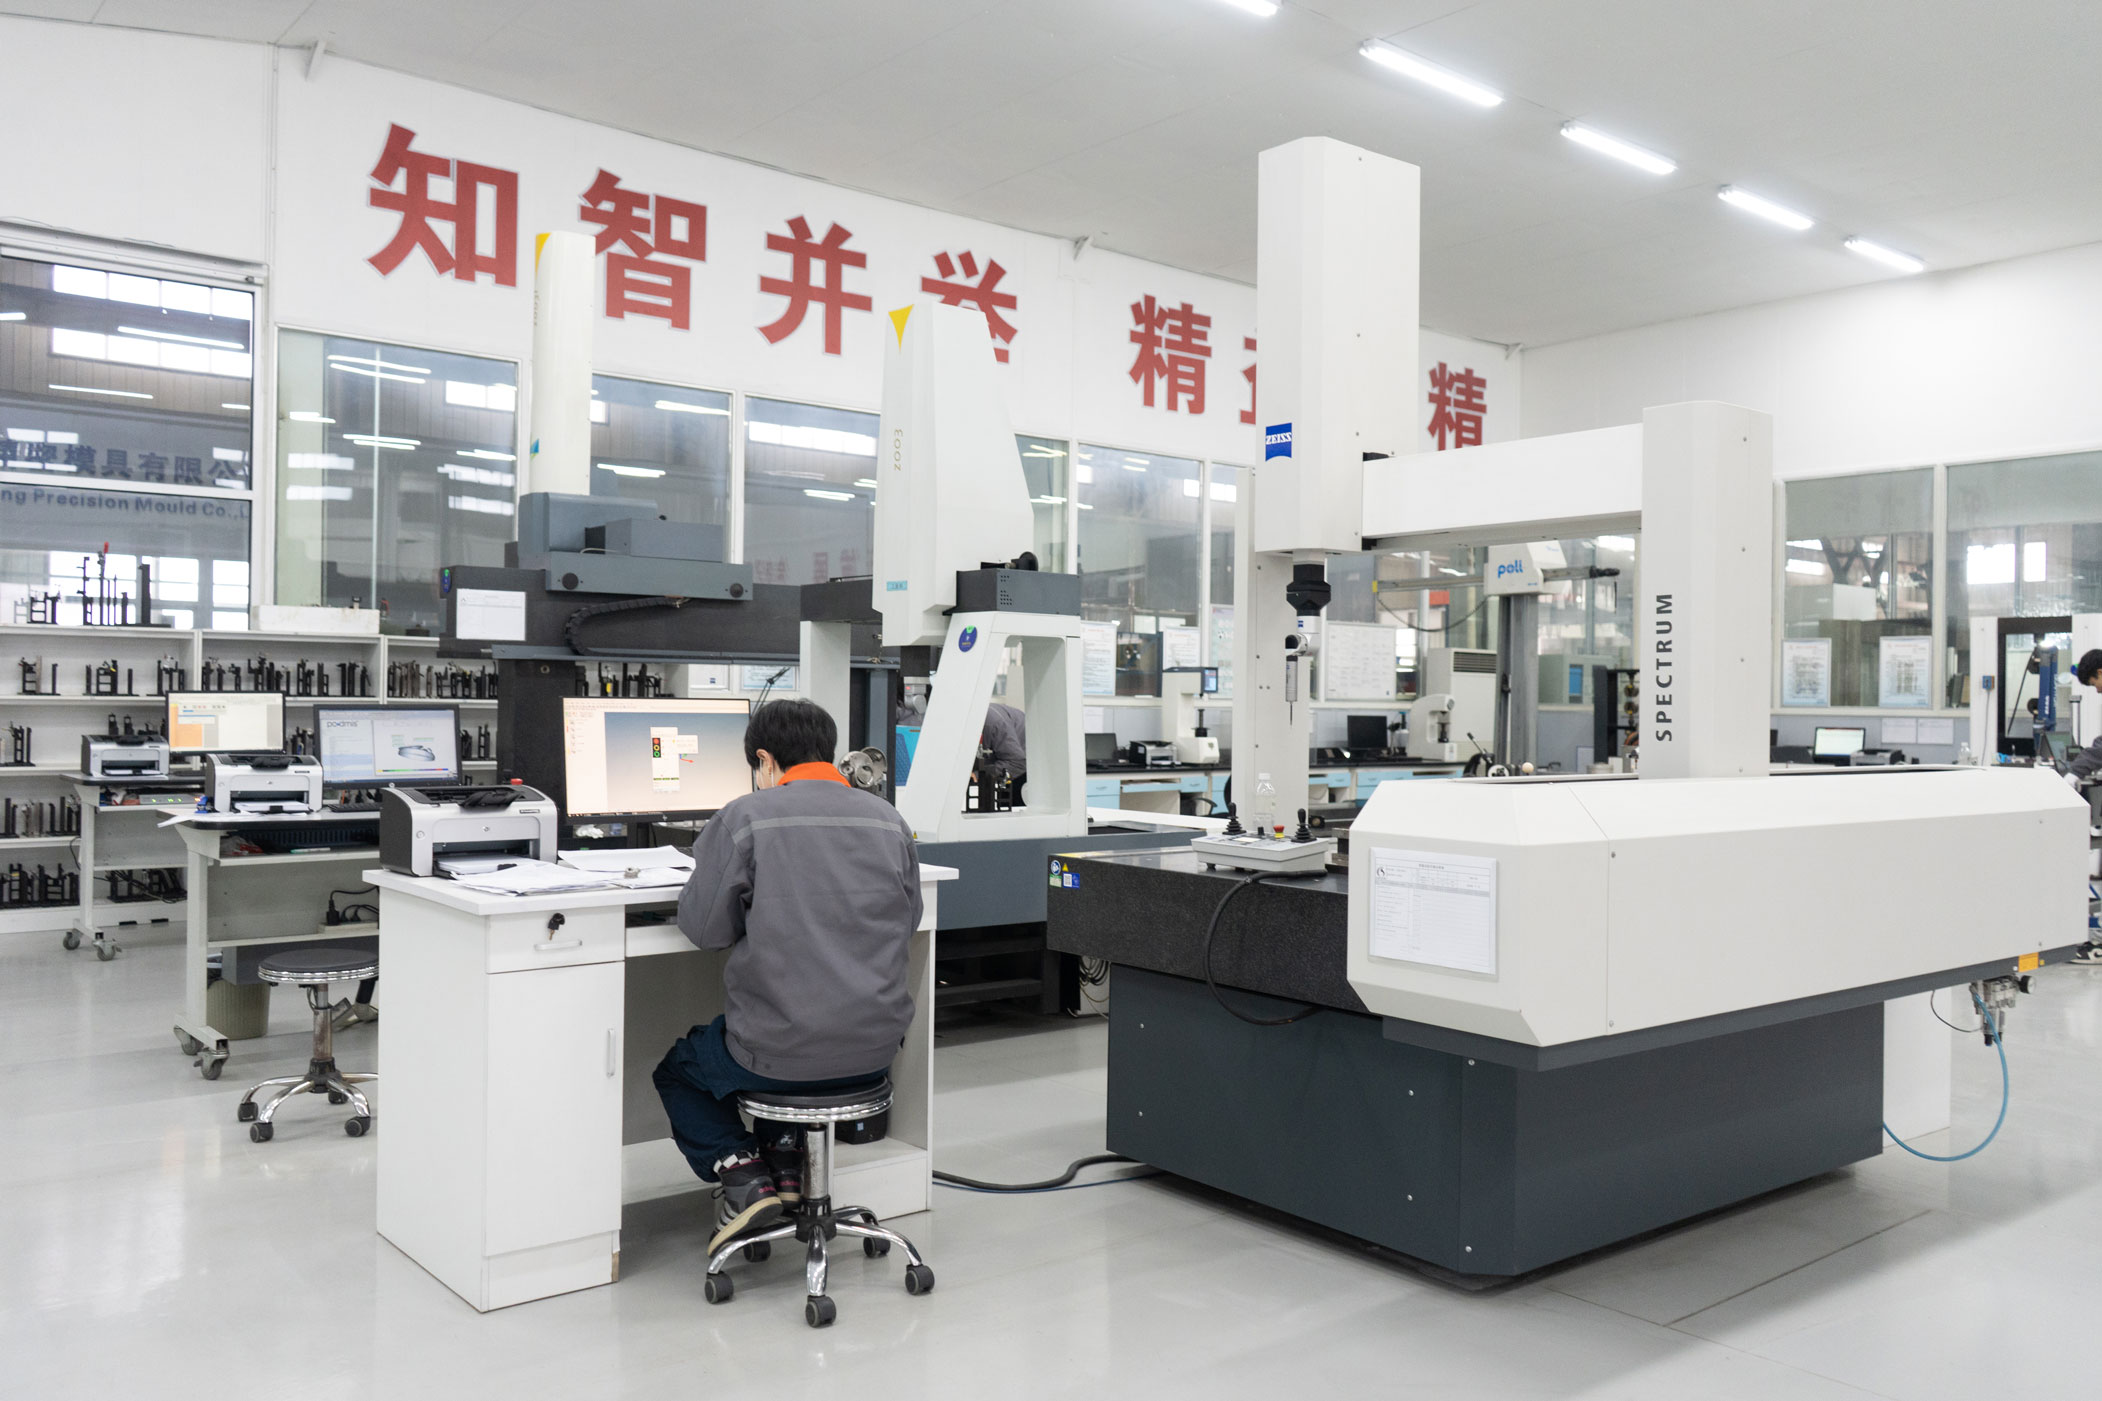
| Inspection records | Who measures final machined dimensions? | Agree on report format before samples. |
| Responsibility | Who owns nonconformance if casting affects machining? | Avoid split accountability. |
A useful scorecard connects commercial discussion to factory reality. If the supplier cannot explain process choice, machining responsibility or inspection records, the quote may still be possible, but the buyer is accepting more risk than the price shows.
RFQ evidence checklist
| RFQ item | Why it matters | Buyer note |
|---|---|---|
| 2D drawing | Dimensions, tolerances, datums, material notes and finish requirements. | Use the latest revision and mark critical features. |
| 3D file | Geometry for tooling, parting line, machining stock and assembly review. | STEP or similar neutral files are usually easier to review. |
| Material grade | Alloy choice, standard, heat treatment and report requirements. | Avoid common names when a formal grade is required. |
| Quantity plan | Prototype, first batch, annual demand and reorder pattern. | Separating sample and production volumes improves tooling decisions. |
| Machining scope | Threads, bores, sealing faces, datums and tight fits. | Clarify what is as-cast and what must be machined. |
| Inspection scope | Critical dimensions, material reports, surface criteria and functional tests. | Attach inspection expectations before sample approval. |
For Waking projects, buyers can start by reviewing CNC machining for cast components, Waking manufacturing capabilities, casting quality inspection requirements, send machined casting drawings for RFQ. These pages give the RFQ conversation a clear path instead of leaving process, machining and inspection as separate topics.
Common mistakes and risk matrix
| Mistake | Why it creates risk | Better practice |
|---|---|---|
| Quoting casting only | The part may be cheap but unusable without machining. | Quote casting and machining together. |
| No datum plan | Machined features can drift relative to casting geometry. | Define datum strategy before tooling. |
| Insufficient machining stock | Cleanup may fail on critical surfaces. | Add practical machining allowance. |
| Separate final inspection | The buyer may receive parts that pass casting checks but fail assembly. | Inspect to final drawing. |
Most sourcing problems begin before production. The drawing is incomplete, machining scope is assumed, inspection criteria are vague, or the supplier and buyer use the same word for different acceptance levels. The solution is not a longer email chain. The solution is a clearer RFQ packet and a supplier that is willing to question unclear details early.
How to use this guide during supplier discussion
Use this article as a working checklist, not as a one-time reading page. The buyer should first mark the non-negotiable requirements: material grade, annual quantity, critical dimensions, functional surfaces, inspection records and shipment conditions. Then compare each supplier response against those requirements. A supplier that gives a fast price but does not discuss process limits may still be useful for a simple part, but it should not be treated the same as a supplier that reviews drawings, machining stock and inspection evidence before quoting.
For production parts, the most important question is often not whether the supplier has a certain machine. The better question is how that machine fits the route from raw casting to approved shipment. A CNC machine does not solve a casting datum problem by itself. A quality certificate does not define which dimensions will be measured. A factory photo does not explain how a drawing revision is controlled. Buyers should turn every broad claim into a practical question: who checks this, when is it checked, what record proves it, and what happens if the sample does not match the drawing?
This is also where internal resources should be used deliberately. If the project is still at process-selection stage, review Waking’s capability and process pages before sending the RFQ. If the project has tight tolerances or mating surfaces, compare the machining scope with the inspection requirements. If the project is close to purchase approval, prepare the RFQ packet and use the related casting and CNC machining articles to check whether any DFM, quality or quoting details are missing. Before finalizing the RFQ, compare this requirement with CNC machining after casting guide, DFM checklist for custom cast parts, casting quality inspection guide so process selection, DFM, quoting and inspection stay aligned. The goal is to make the supplier response easier to compare, not simply longer.
Signals that the quote is becoming reliable
- The supplier repeats the material grade, process route, machining scope and drawing revision back to the buyer.
- The quote separates tooling, sample, machining, surface finish, inspection, packaging and freight assumptions where relevant.
- The supplier identifies at least one risk or clarification question instead of pretending every drawing is ready.
- Inspection expectations are visible before sample production, including critical dimensions and documentation requirements.
- The commercial contact can explain what engineering still needs before final price or delivery promises are fixed.
Aligning purchasing, engineering and quality
Before the buyer sends the final RFQ package, someone should check that purchasing, engineering and quality are asking for the same result. Purchasing may focus on price and delivery, engineering may focus on fit and function, and quality may focus on inspection records. A casting project works better when those requirements are visible in one packet. If one department keeps a requirement only in email, the supplier may miss it during tooling, sampling or shipment preparation.
For repeat orders, keep a short record of what was learned from the first sample: drawing notes that caused questions, dimensions that needed tighter control, packaging details that protected machined surfaces, and reports the buyer actually used. That record makes the next RFQ faster and gives the supplier a clearer target for stable production.
Procurement checklist
| Timing | Action |
|---|---|
| Before RFQ | Collect drawings, CAD, material, quantity, finish and inspection notes. |
| Before tooling | Confirm DFM feedback, process choice, tooling assumptions and sample approval plan. |
| Before samples | Agree on report format, measured dimensions, surface criteria and packaging. |
| Before production | Freeze drawing revision, tolerance interpretation, delivery terms and change-control rules. |
| Before shipment | Check inspection records, material documents, labels, packaging and invoice details. |
- Confirm whether the part is mainly a casting problem, a machining problem, or a combined casting-machining problem.
- Mark critical dimensions separately from general dimensions so inspection effort goes where it matters.
- State whether samples need dimensional reports, material reports, photos, assembly checks or functional tests.
- Ask how drawing changes are controlled after tooling starts.
- Keep packaging and shipping requirements visible if the part is heavy, machined, coated or corrosion-sensitive.
Authority sources
- Google Search Central helpful content guidance
- ISO 9001 quality management
- ASTM standards
- ASME Y14.5 dimensioning and tolerancing
- NIST manufacturing and measurement resources
FAQ
Why source casting and machining together?
It reduces handoff risk because the supplier can plan tooling, stock, fixtures and final inspection as one route.
Which features usually need machining?
Bearing seats, mounting faces, threads, bores, sealing surfaces and datum faces often need CNC machining after casting.
Can machining fix all casting variation?
No. Machining needs enough stock and stable datums. Poor casting control can still create scrap.
What should a machined casting RFQ include?
Include drawings, CAD, material, quantity, machined features, tolerance priorities, finish, reports and packaging needs.
Frequently Asked Questions
What drawing and file information should I provide so the supplier can quote cast-and-machine scope without assumptions?
Provide the latest-revision 2D drawing with dimensions, tolerances, datums, material notes and finish requirements, plus a 3D file for geometry, parting line and machining stock review. Mark as-cast surfaces and machined features clearly, and list threads, bores, sealing faces and tight fits. This prevents separate sourcing gaps.
How do I specify machining allowance to prevent cleanup failure?
The guide says insufficient machining stock risks cleanup failure on critical surfaces, so you should define a practical machining allowance. The exact allowance depends on casting process, part size and tolerance requirements, and must be confirmed with the factory for each part.
What final inspection records should I request for machined casting components?
Request CMM dimensional reports measured against drawing datums, material certificates with batch traceability, and first article inspection or sample approval. For pressure applications, ask about leak testing. Agree on the report format before samples so you do not receive parts that pass casting checks but fail assembly.
How can I avoid split accountability when casting defects affect machining or final dimensions?
Treat casting and CNC machining as one manufacturing route. Ask the supplier to confirm who owns nonconformance if casting affects machining, and verify that machining responsibility and inspection records are explained in the quote. Waking performs casting, machining and inspection in one factory, which reduces split accountability.
Key Parameters at a Glance
| Parameter | What to specify in the RFQ | Waking factory evidence |
|---|---|---|
| Drawing and 3D data | Latest 2D drawing with datums, tolerances, surface finish and critical features; 3D file for stock and geometry review | Engineering review and quotation review drawing before quoting |
| Material grade | Formal alloy grade and material report requirements; avoid common names | Stainless steel 304/316/CF8/CF8M; carbon steel; alloy steel; aluminum alloy |
| Casting process route | Define as-cast surfaces vs machined features; clarify casting method for tooling | In-house investment casting, low-pressure aluminum casting, gravity aluminum casting |
| Machining scope | Threads, bores, sealing faces, datums and tight fits must be listed | 400+ in-house CNC machines in the same factory as casting |
| Inspection records | CMM dimensional reports, material certificates, FAI, sample approval, leak testing if needed | CMM COORD3/ZEISS SPECTRUM, X-ray XTH320, batch traceability and material certificates |
