
CNC Machined Castings — One Factory From Foundry to Finished Part
Casting + CNC Since 2002 | ISO 9001 & IATF 16949 | X-Ray Before the Cutter | 400+ CNC Machines In-House
Quote Casting + Machining
🔒 Used only to reply to your inquiry — no spam, never shared.
Cast, Then Machined — In the Same Plant
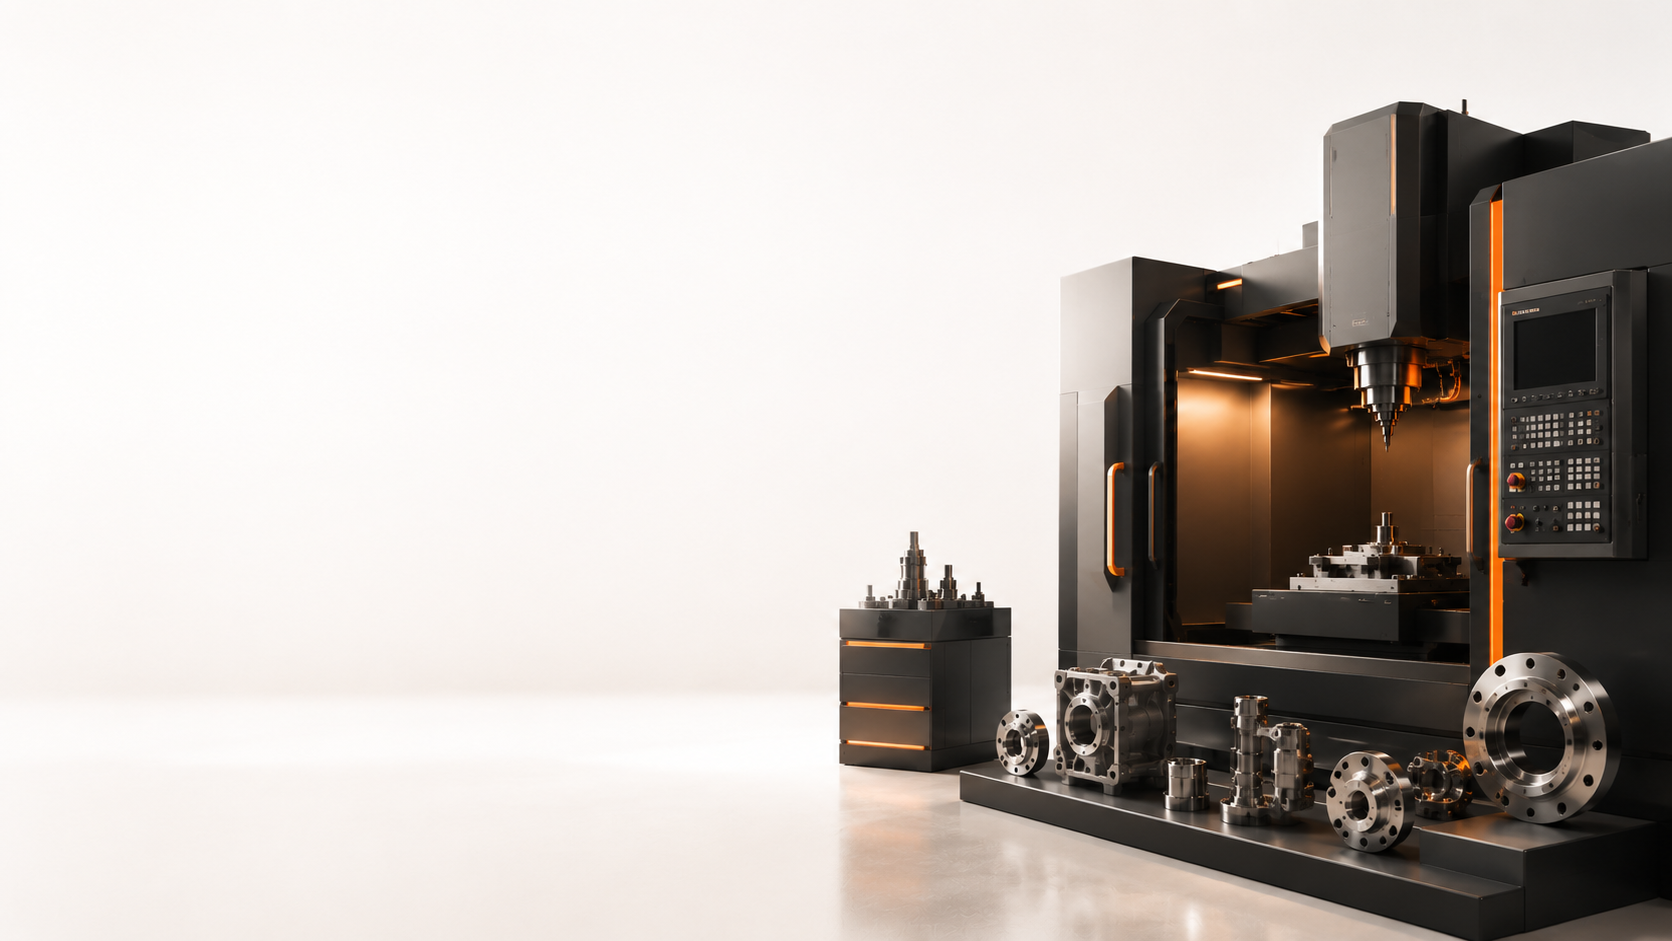
Machined Investment Castings
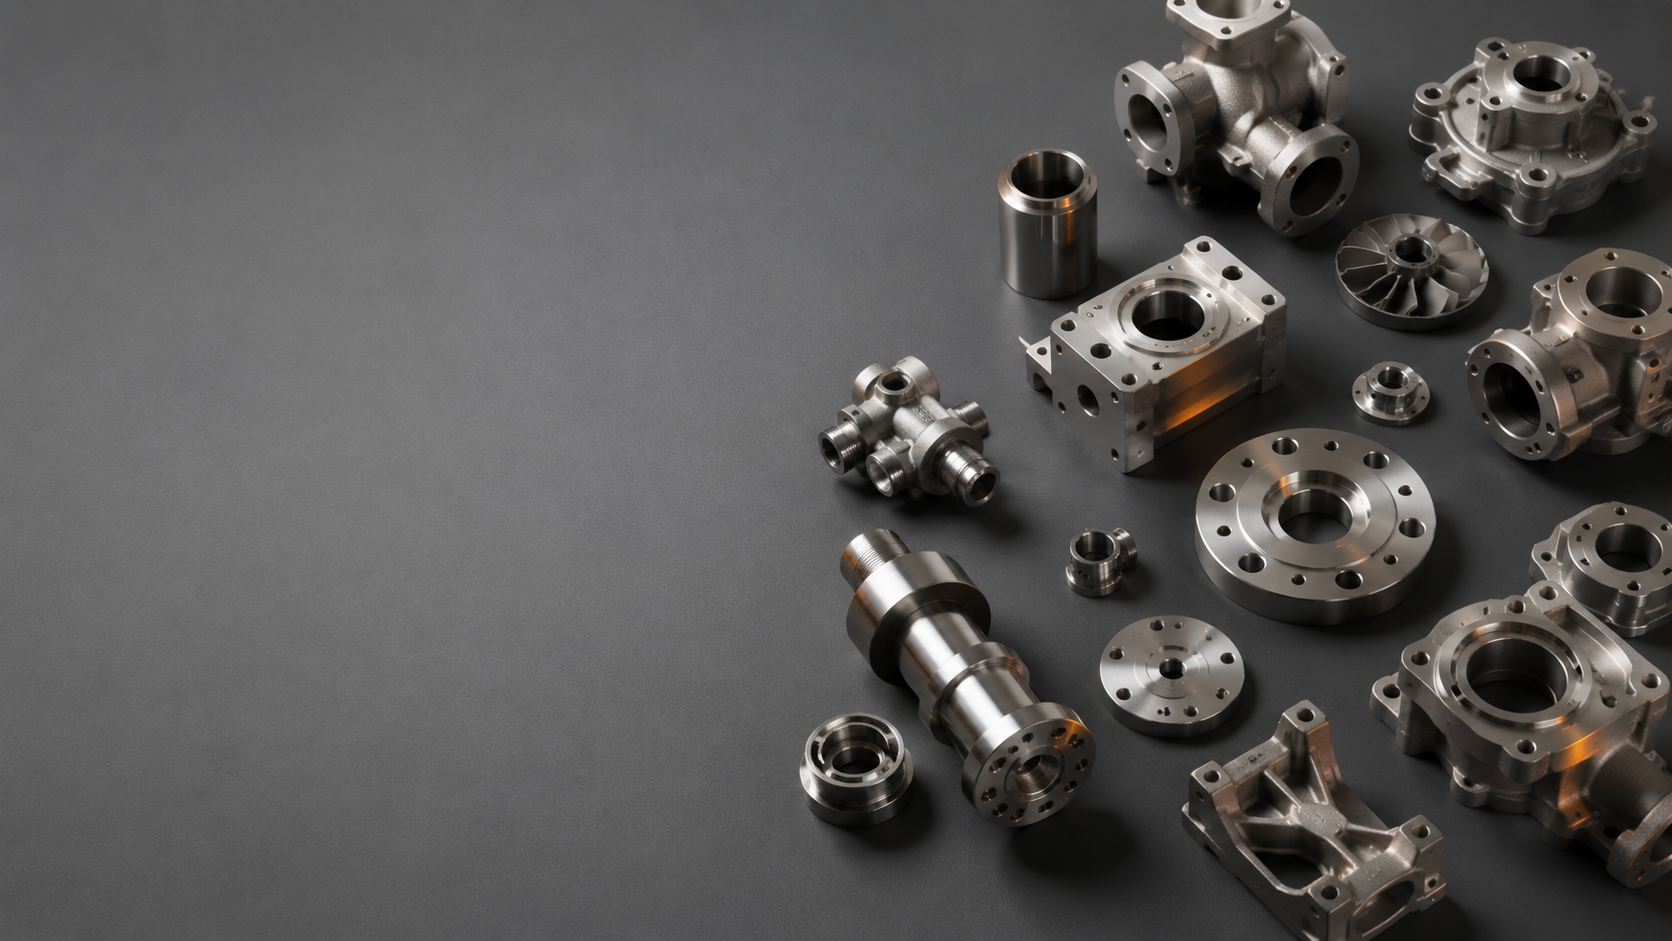
Valve Bodies & Pump Parts
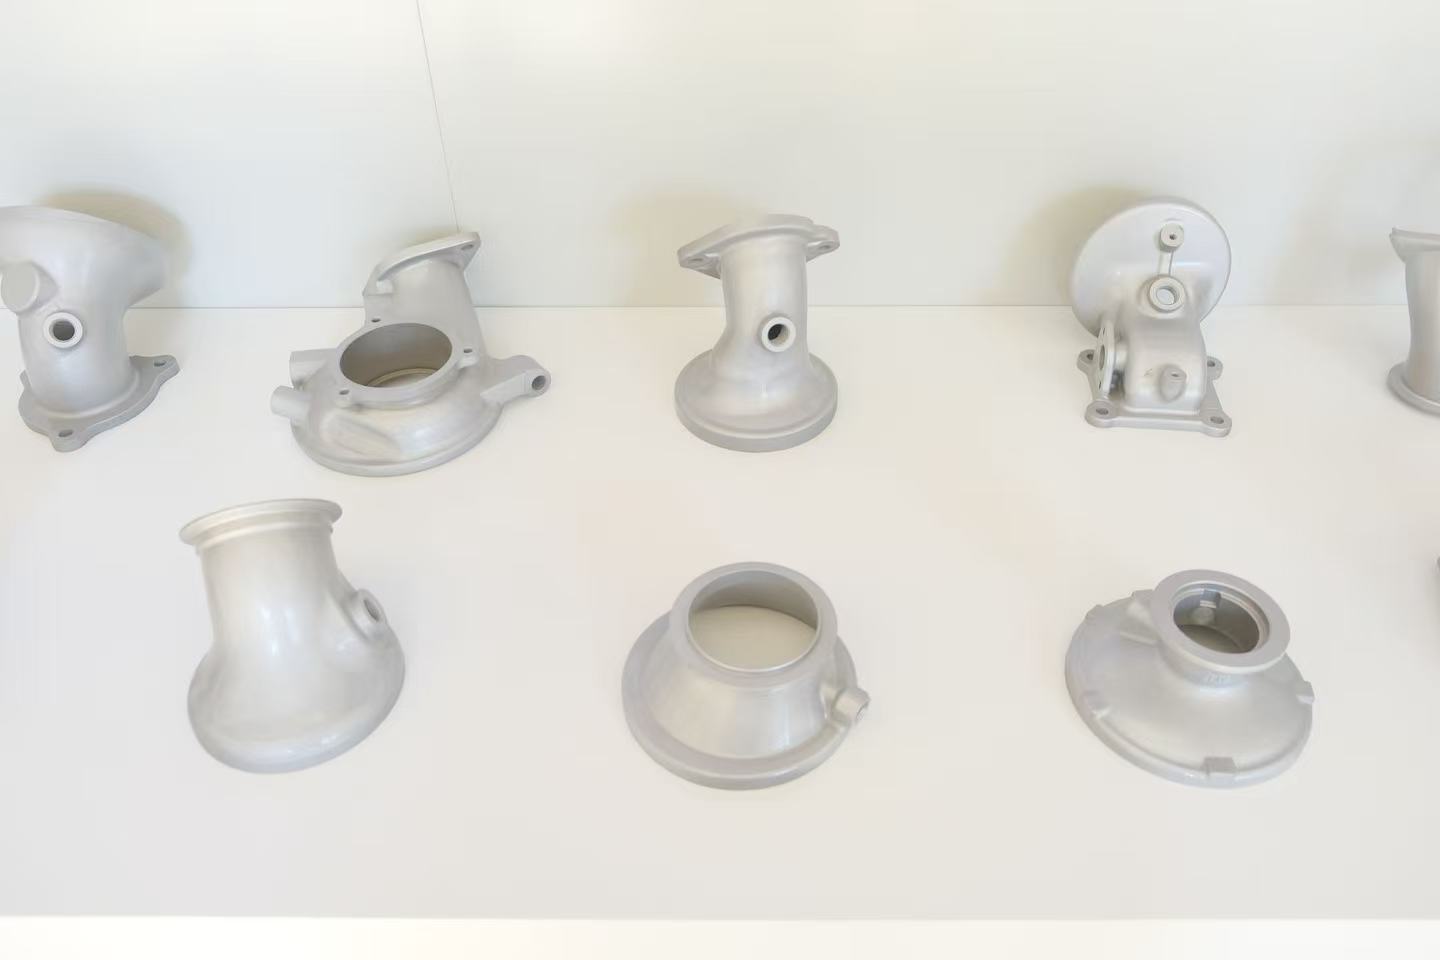
Machined Aluminum Housings
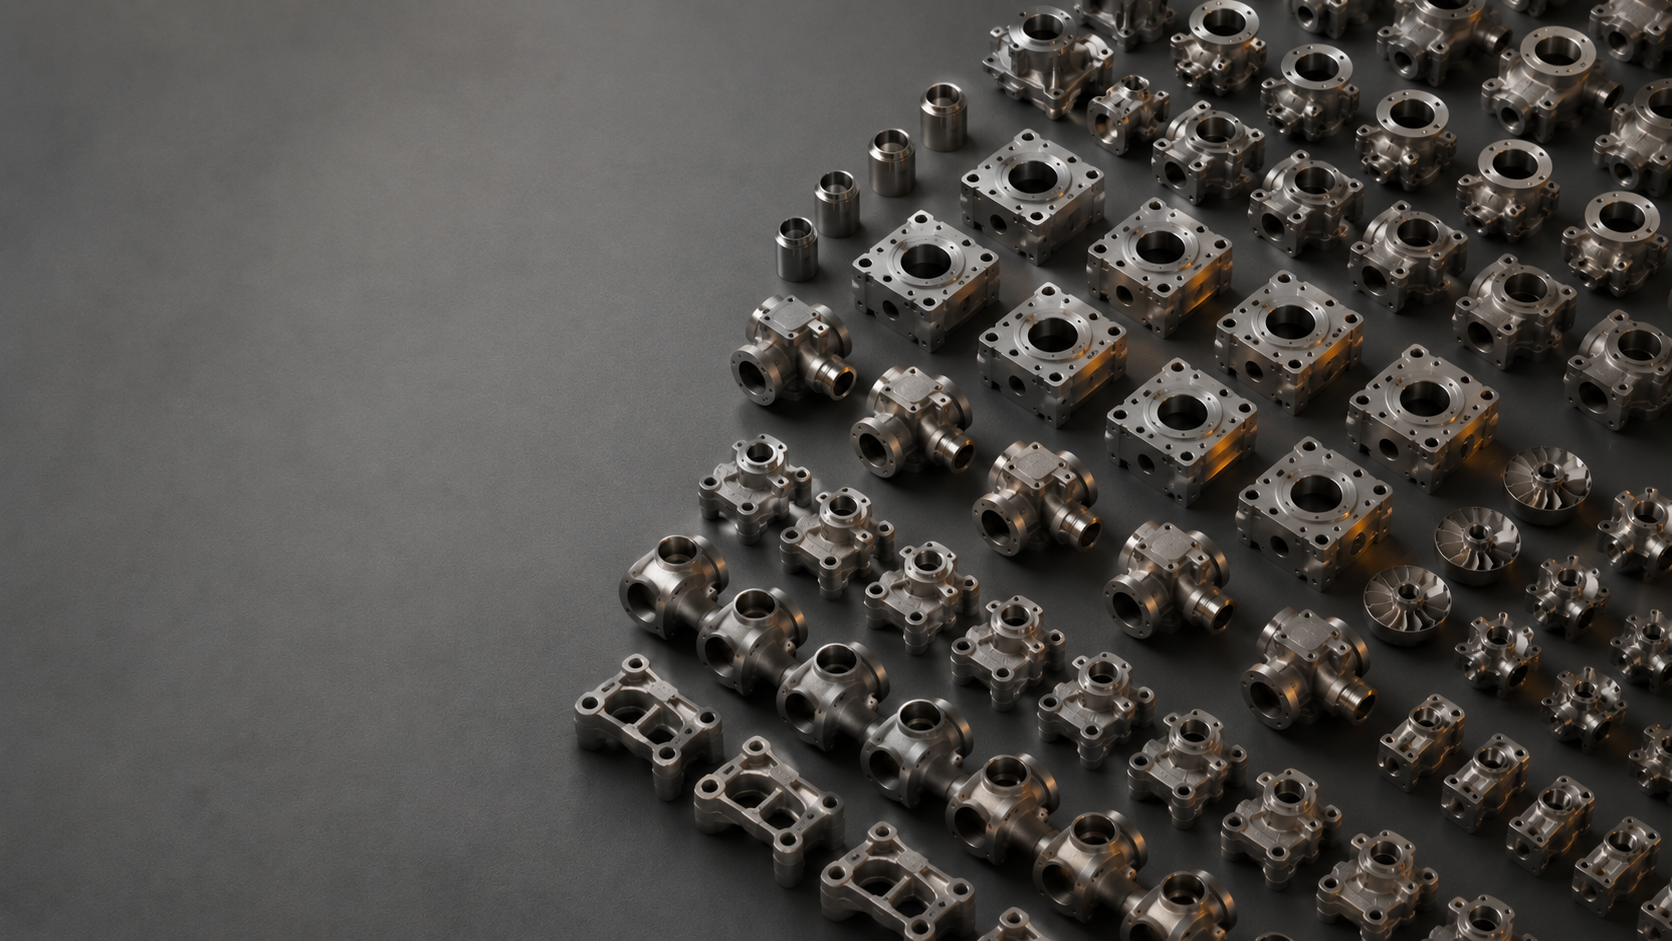
Steel Machinery Components
Investment castings and aluminum castings with in-house CNC machining — X-ray screening before the cutter, CMM verification after it, one supplier responsible for the finished part
Why Cast + Machine Belongs in One Factory
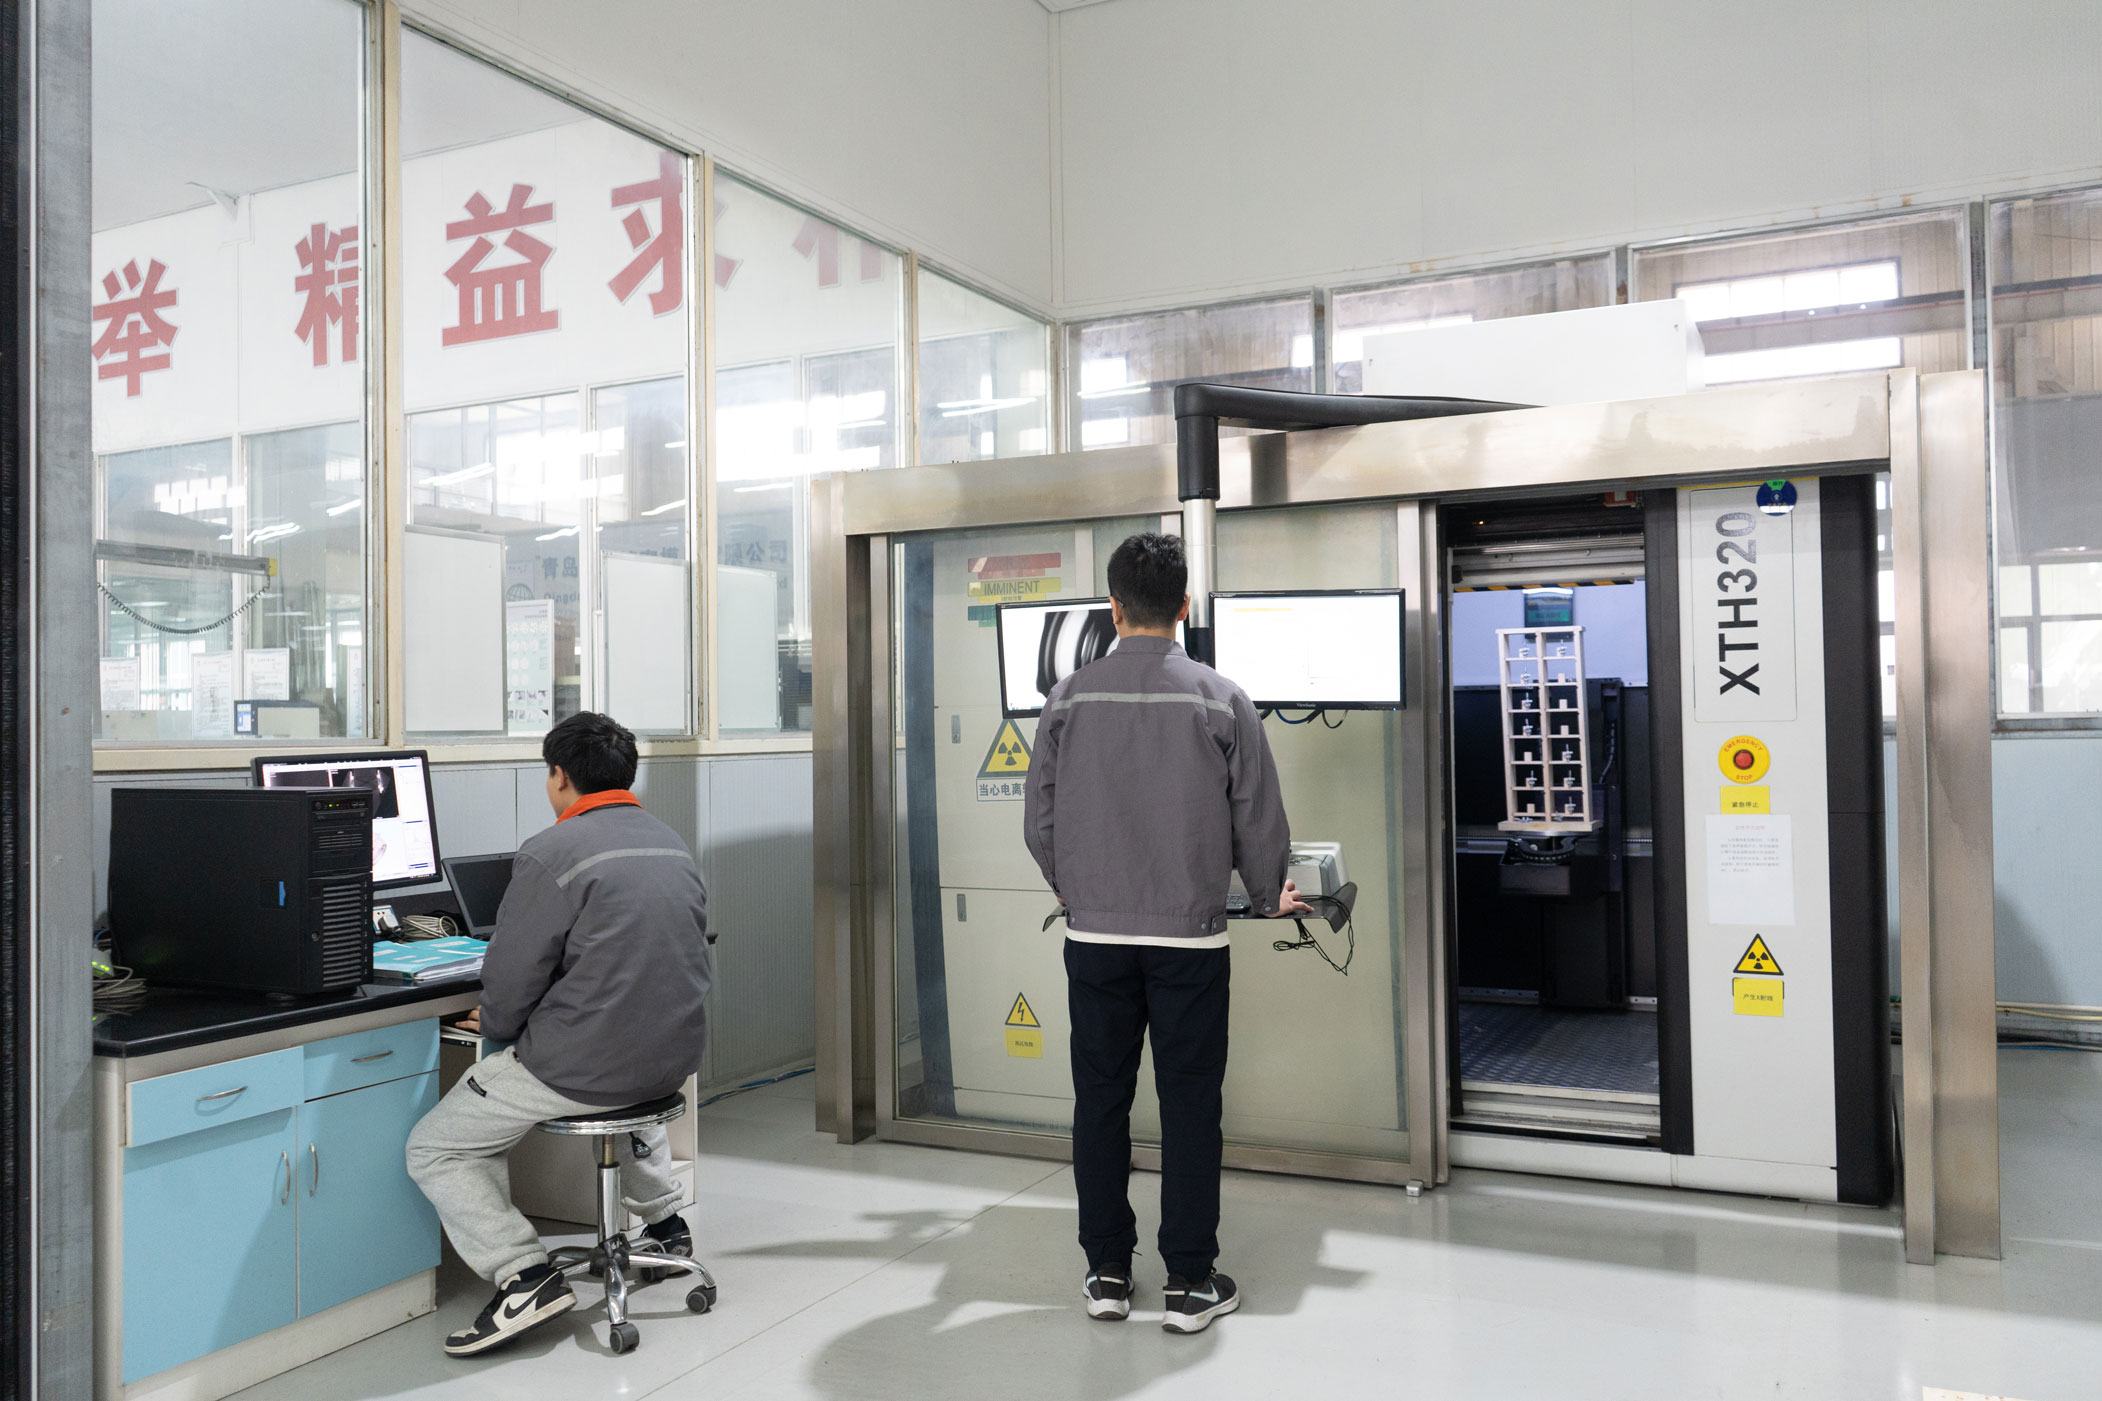
X-Ray Before the Cutter Touches Metal
The most expensive casting defect is the one you machine. Subsurface porosity and shrinkage are invisible on an as-cast surface — until a finishing pass opens them up on a sealing face, and the part scraps after machining time has been paid. Our XTH320 X-ray NDT system screens structural and pressure-critical castings before they reach the CNC floor, so defective castings are caught at foundry cost, not at machined-part cost.
| Screening | XTH320 X-ray NDT before machining |
| Targets | Gas porosity, shrinkage, inclusions |
| When | Sample approval and per inspection plan in production |
| Benefit | Defects caught at casting cost, not after machining |
| Follow-up | Leak testing on pressure-containing parts |
Datums and Allowances Planned Together
When casting and machining are quoted by two companies, machining allowance is a guess and datum strategy is an argument. Here they are one plan: the engineers who design the gating also set the machining stock and the datum sequence, so the first machined face establishes a reliable zero and every later operation references it. Castings move from the foundry to 400+ CNC machines without leaving the site — no freight between vendors, no translation loss between drawings.
| Machining | Milling, turning, drilling, tapping on 400+ machines |
| Planning | Allowance and datum strategy set at casting review |
| Fixturing | Casting-specific fixtures for distortion control |
| Typical features | Sealing faces, bearing bores, threads, flange faces |
| Result | One party responsible for the finished tolerance |
Sealing Faces and Leak-Tight Parts
For valve bodies, pump housings and anything that holds pressure, the casting gives you the body and the flow path — machining gives you the surfaces that actually seal. We machine seats, flange faces and O-ring grooves in-house, then leak test pressure-containing parts as part of the flow. If a sealing face must be porosity-free after machining, write it on the drawing: that requirement drives our X-ray plan, our stock allowance and our inspection points.
| Parts | Valve bodies, pump housings, pressure components |
| Materials | Stainless 304 / 316 / CF8 / CF8M, steel, aluminum alloy |
| Machined features | Seats, flange faces, grooves, mounting planes |
| Verification | Leak testing built into the production flow |
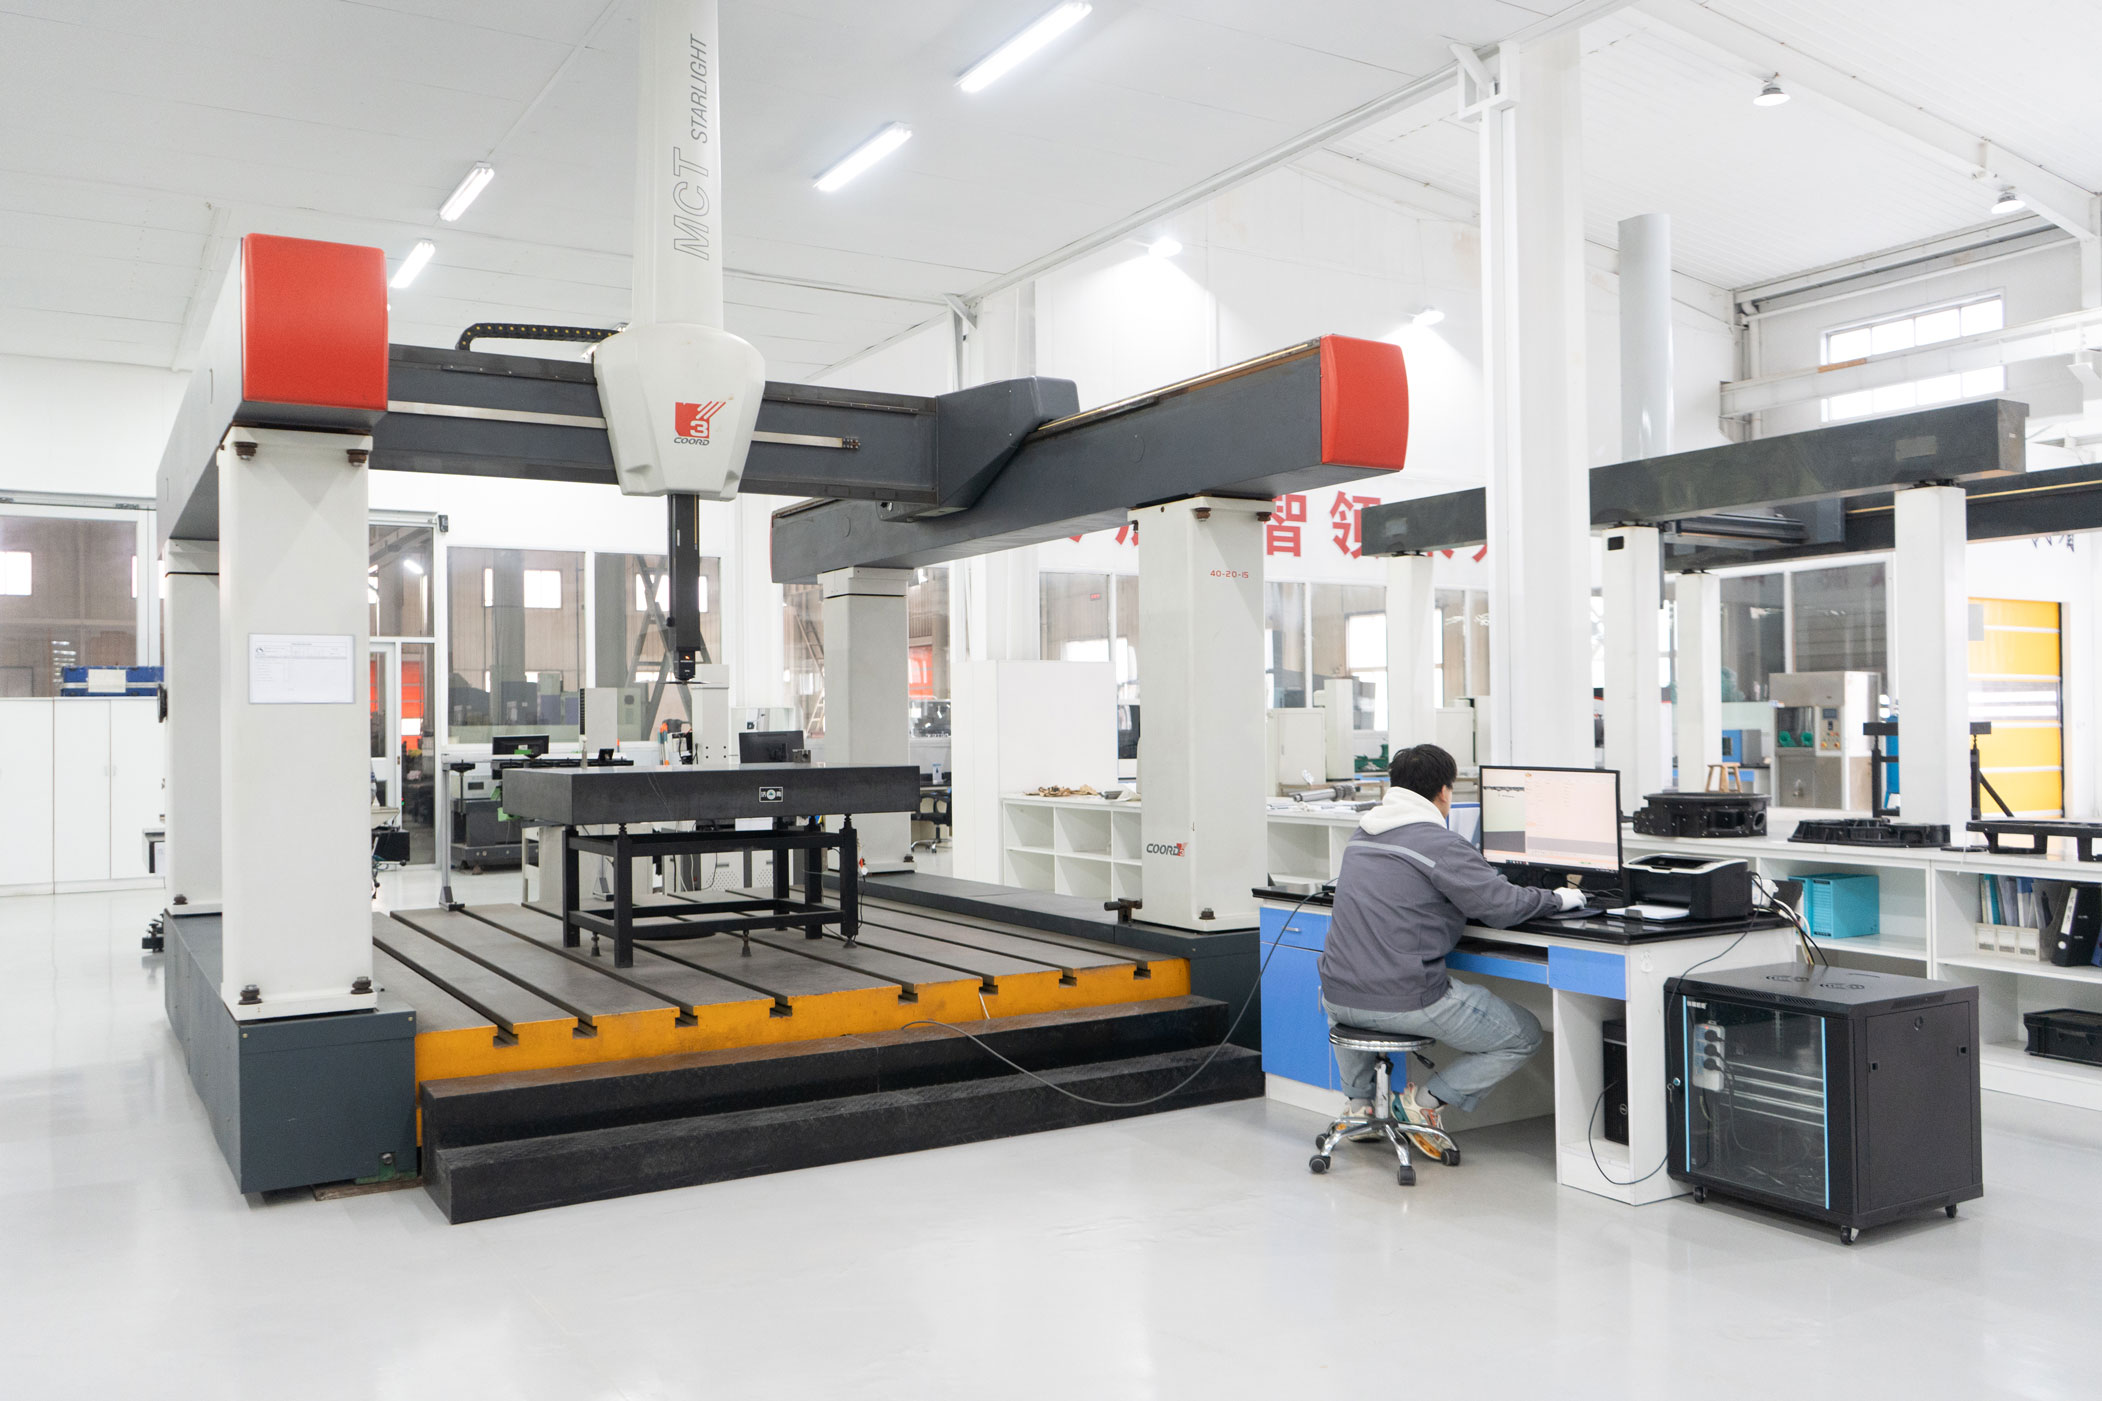
| Dimensional | CMM checks on COORD3 & ZEISS SPECTRUM |
One Report Set for the Finished Part
Buy the casting and the machining separately and your paperwork arrives in pieces — a material cert from one company, a dimensional report from another, and a gap in between when something fails. Here the batch record follows the part through the whole route: melt, heat treatment, machining, final inspection. Material certificates and inspection reports are issued together, traceable to the batch, from one supplier your QA team can actually audit.
| Traceability | Batch-level, melt to finished part |
| Documents | Material certs + dimensional reports, one source |
| First article | FAI on machined features before production |
| Sample approval | Locked before volume production starts |
| System | ISO 9001 & IATF 16949 certified plant |
A casting can pass every dimensional check and still fail as a finished part — porosity hides under the skin until the cutter exposes it, and a machinist working from as-cast datums inherits every casting variation. These problems are only cheap to fix when the foundry and the machine shop share a floor.
The Handoff Problem, Solved by Not Having One
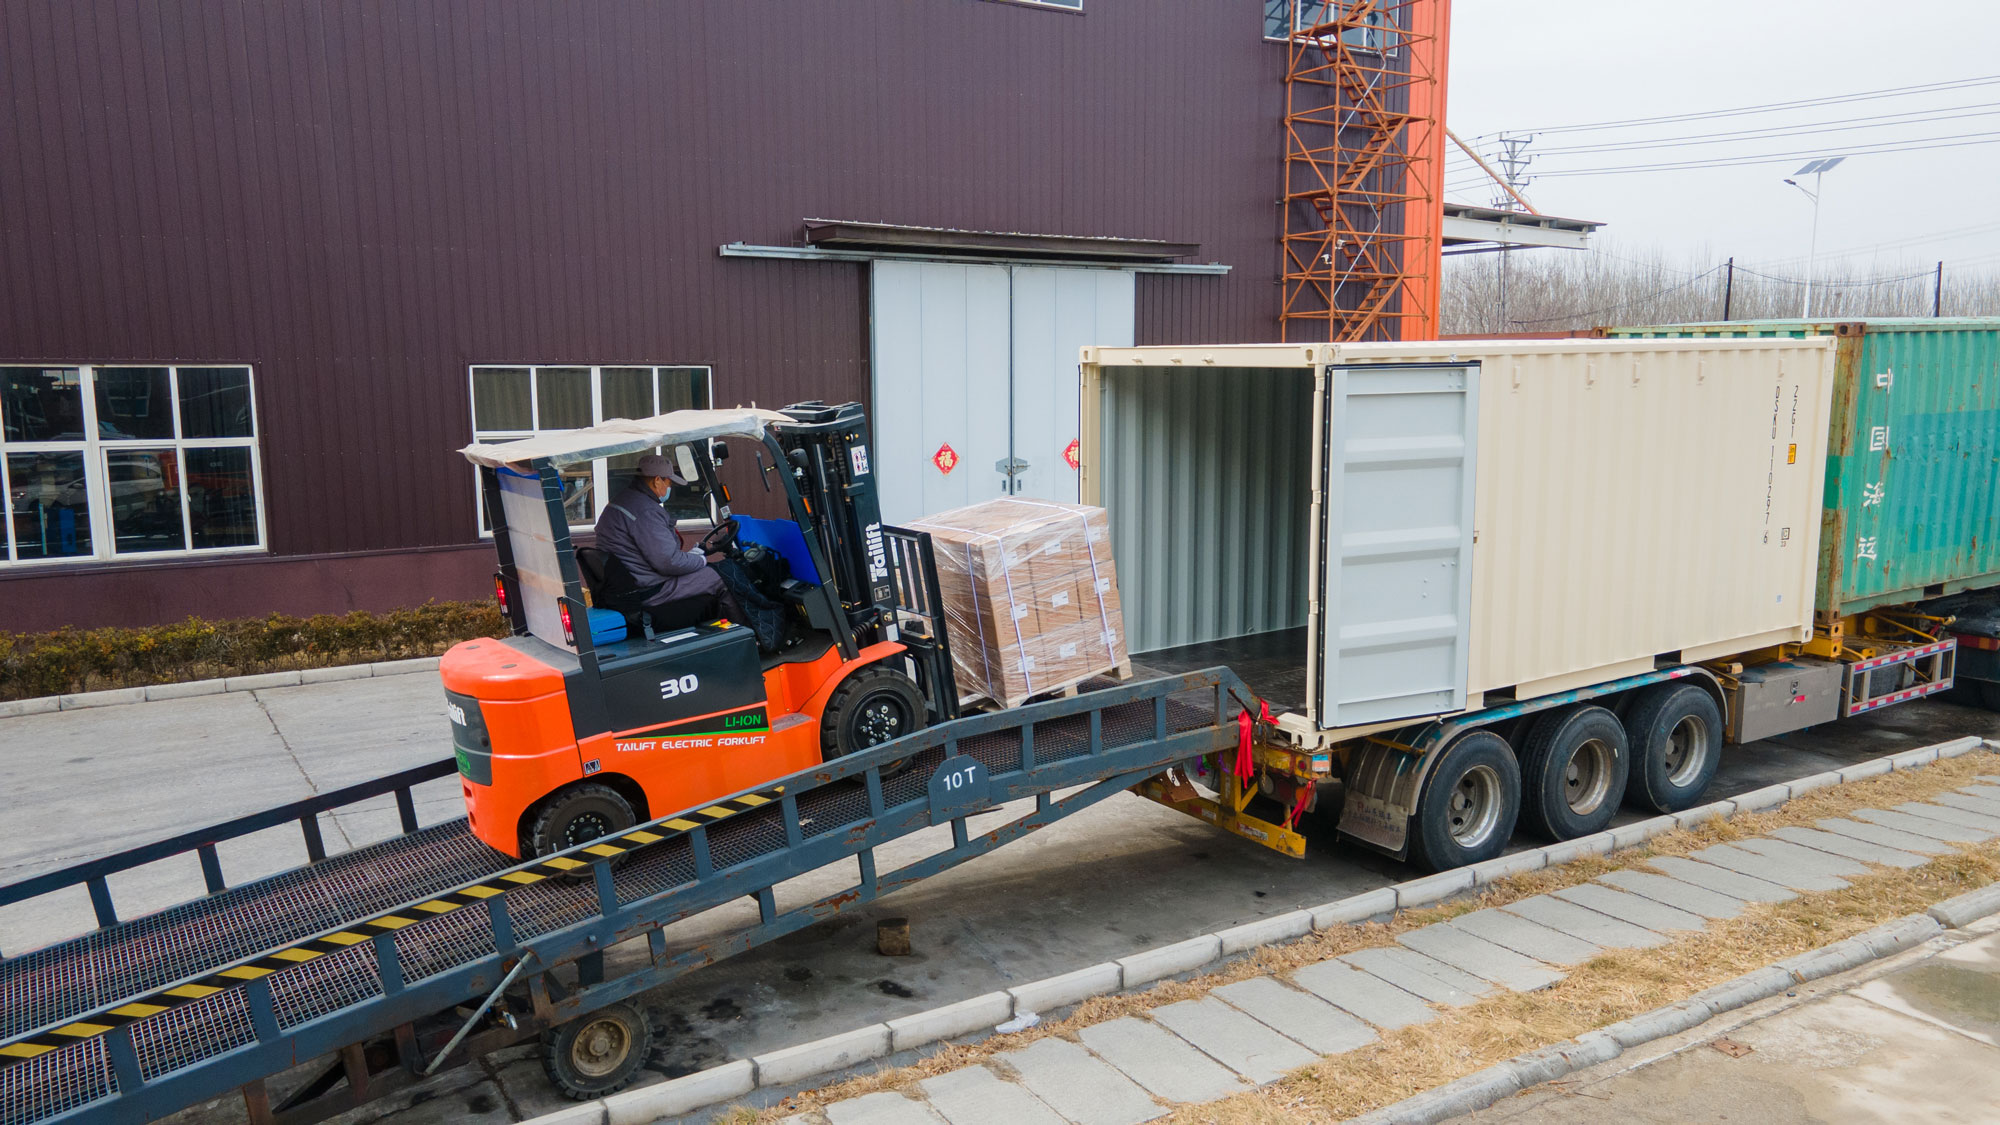
Ask anyone who has bought castings machined by a second vendor: when a bore runs out of tolerance, the foundry says the casting was in spec and the machine shop says the casting moved. Both are right, and the buyer pays. Since 2002 Waking has run the foundry and the machine shop on one 70,000 m² site in Qingdao — the casting engineers and the CNC programmers work from the same review, measure with the same lab, and answer to the same name on your purchase order.
- Casting and machining quoted, planned and produced together
- X-ray screening before machining, CMM verification after
- ISO 9001 quality management · IATF 16949 certified
- Export packing and batch documentation from one source
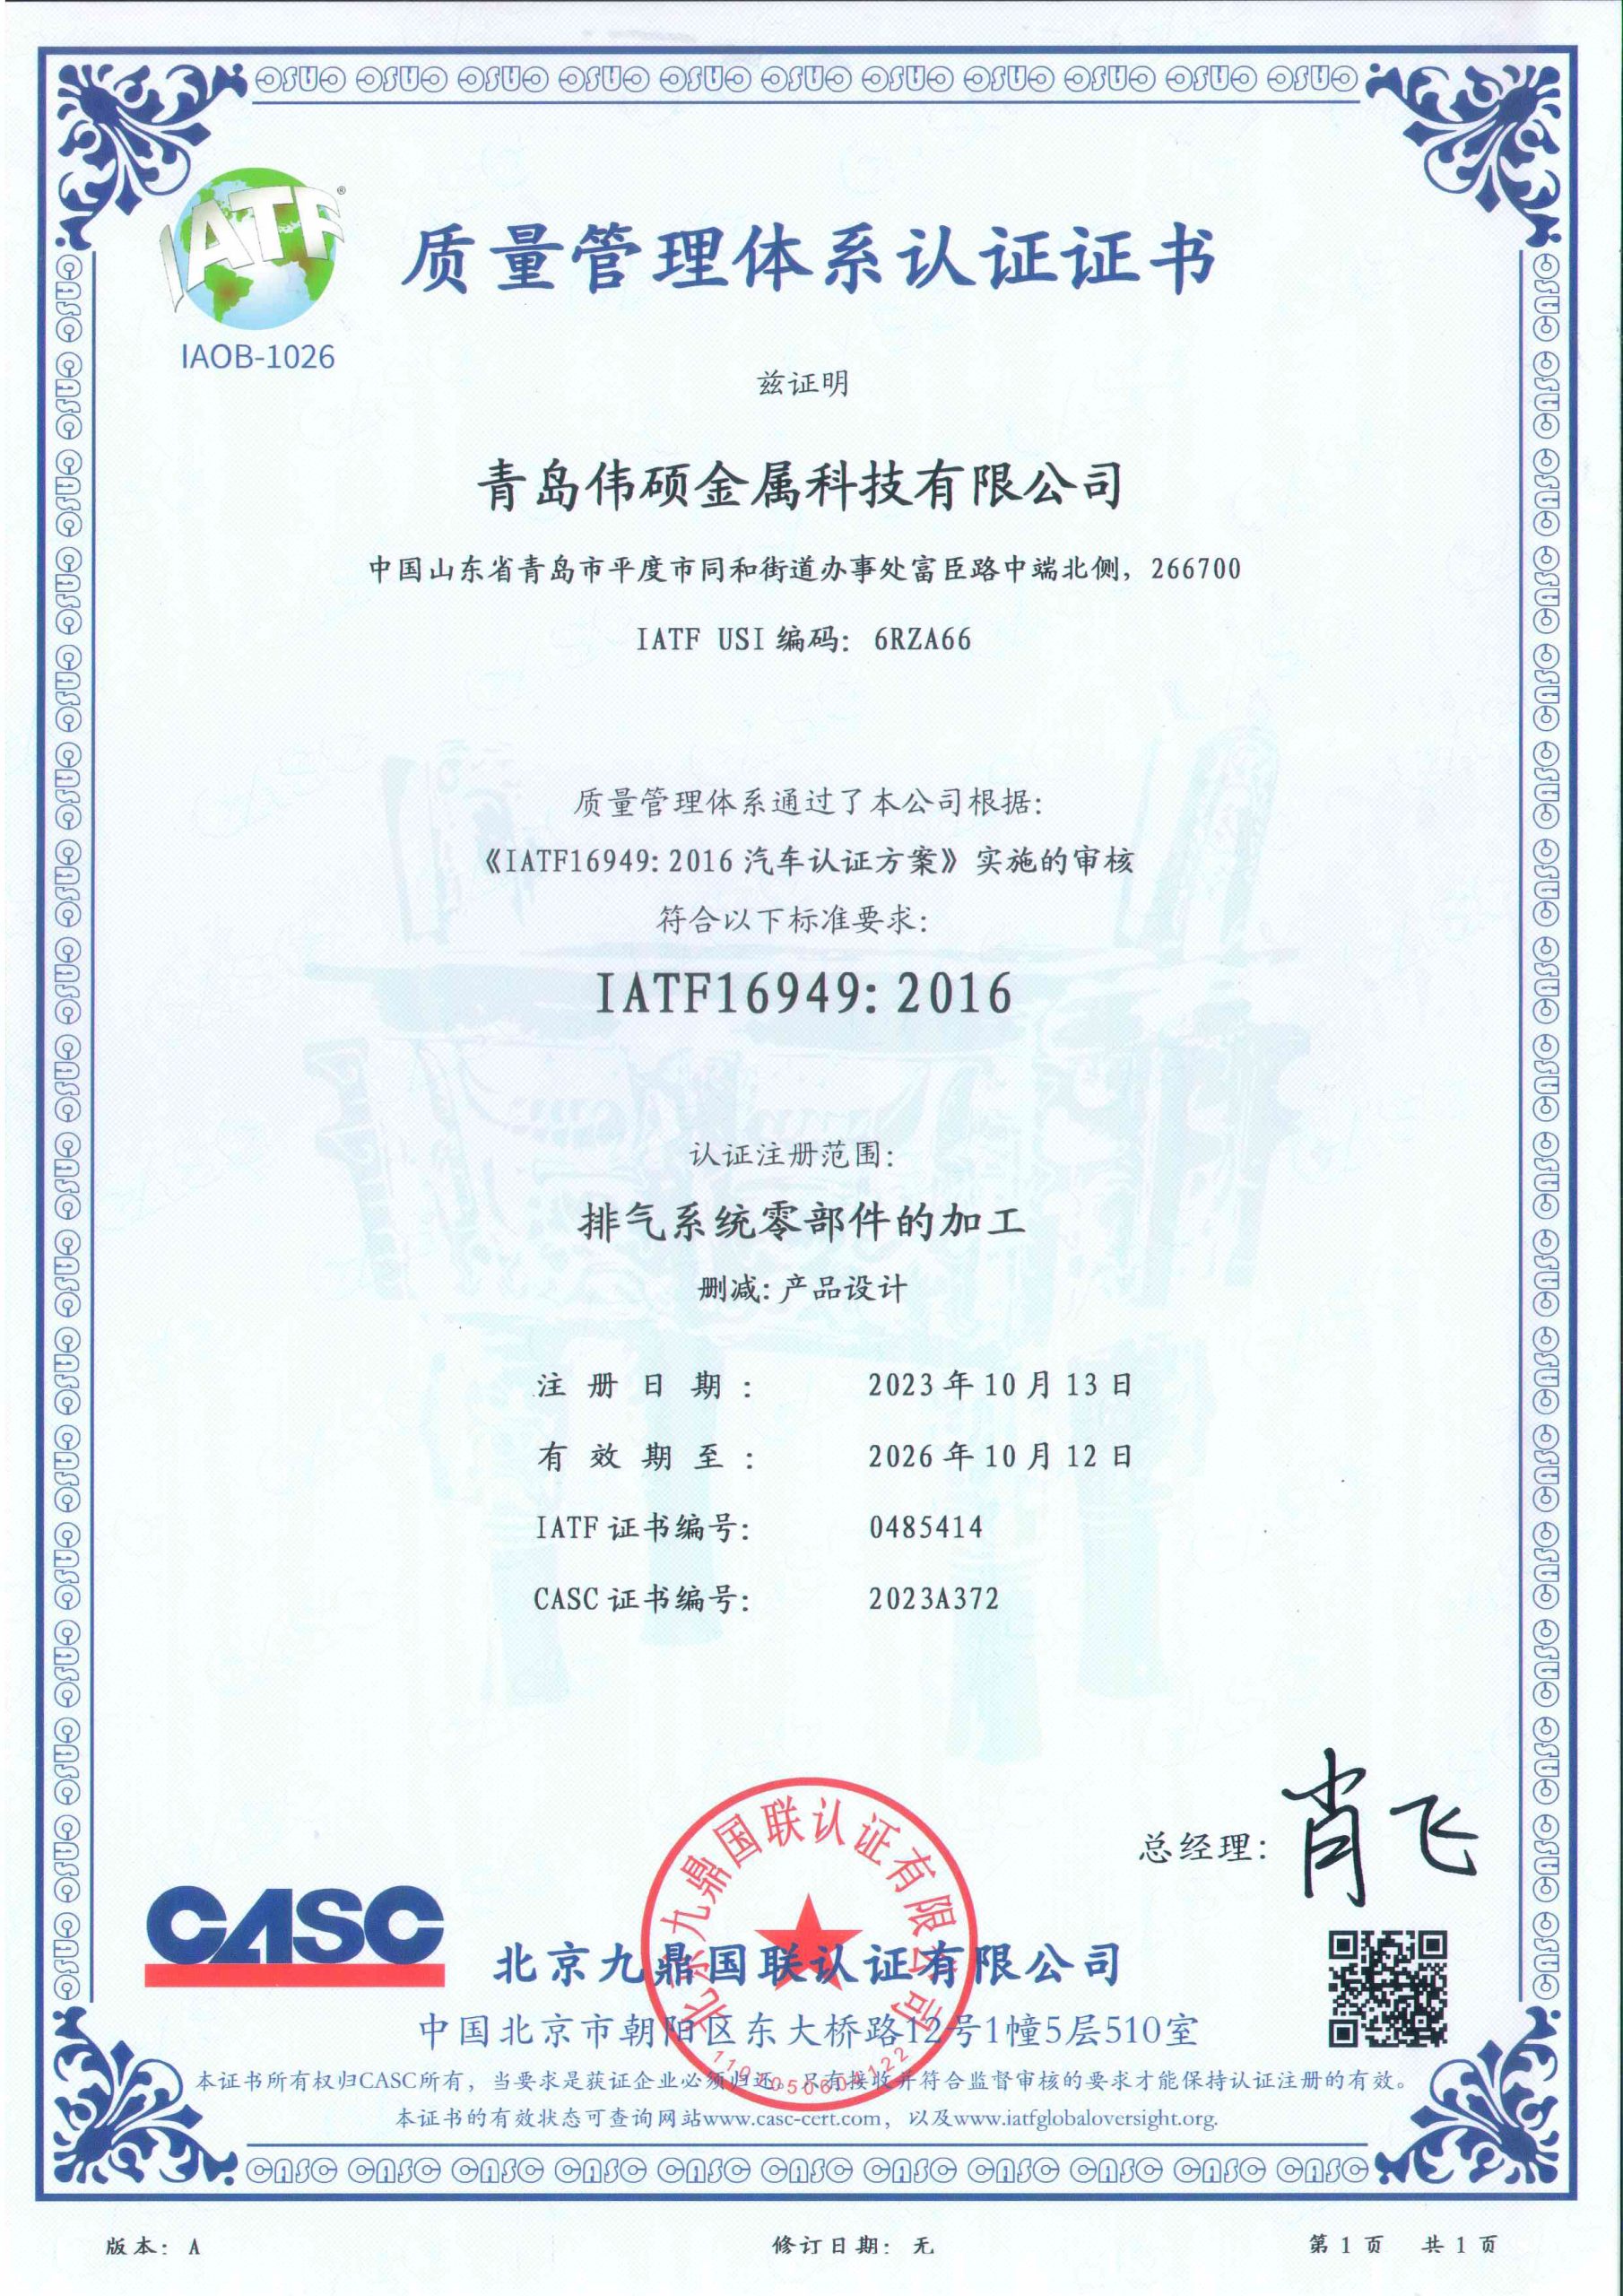
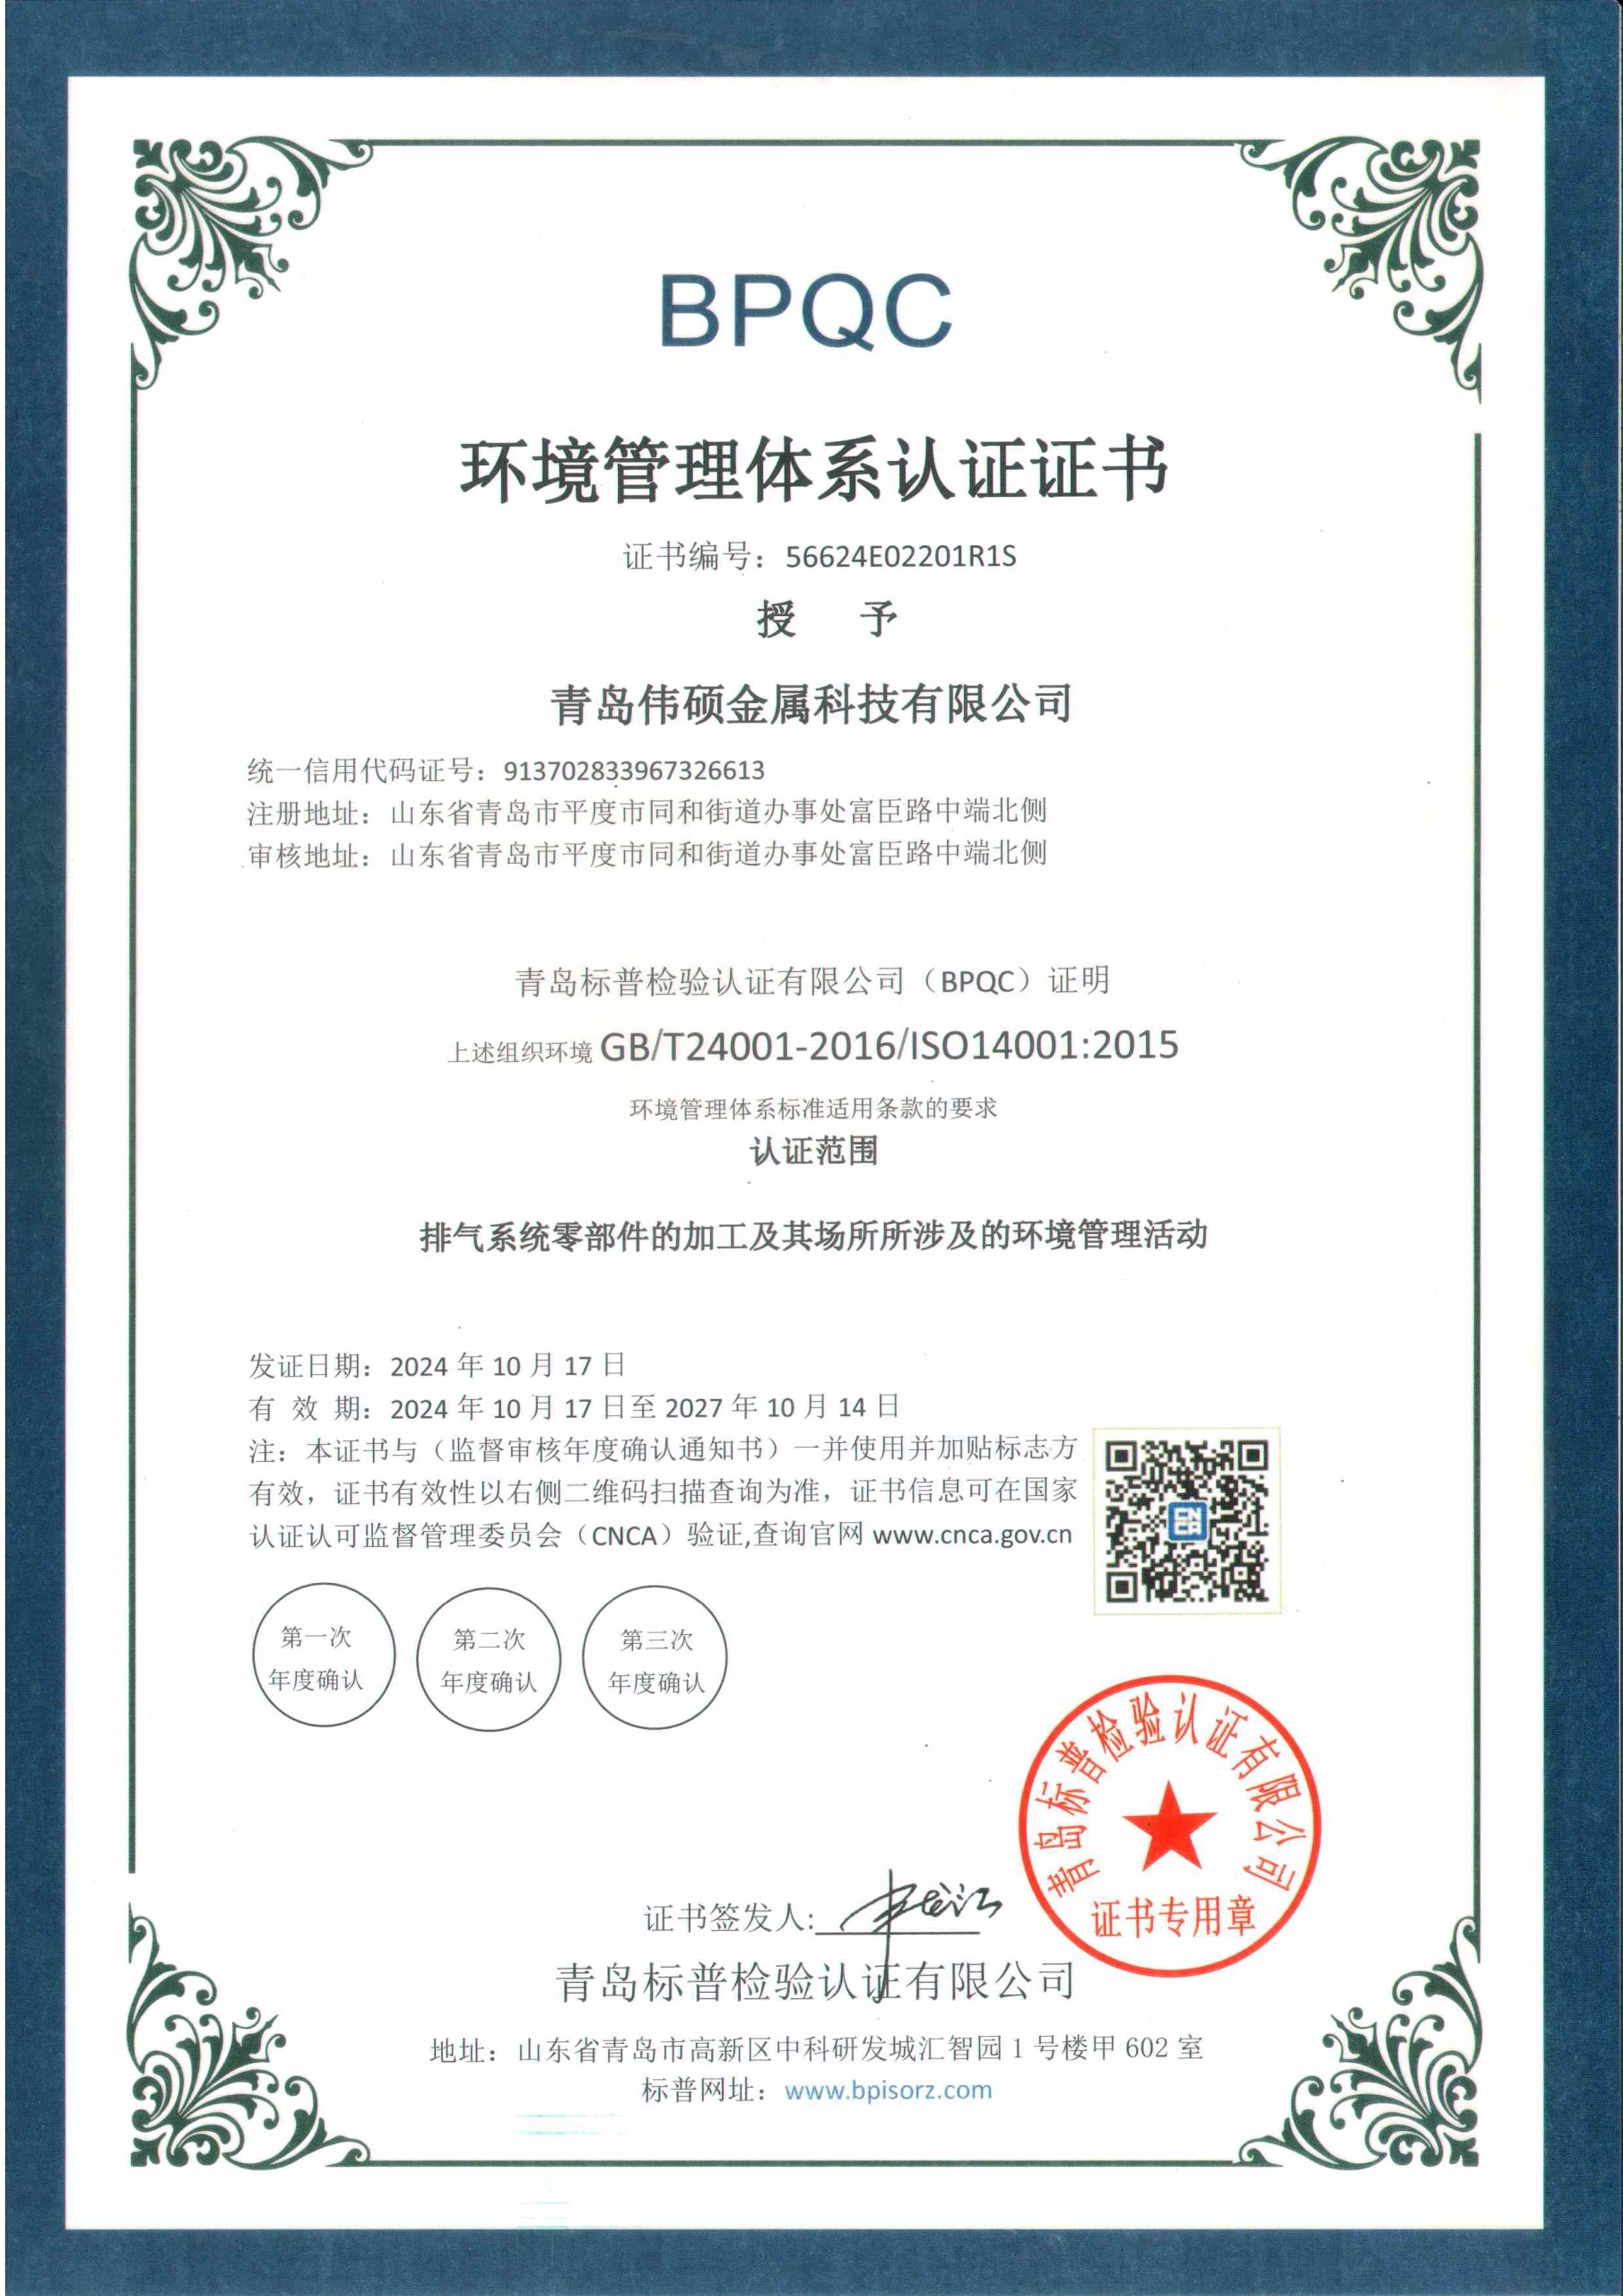
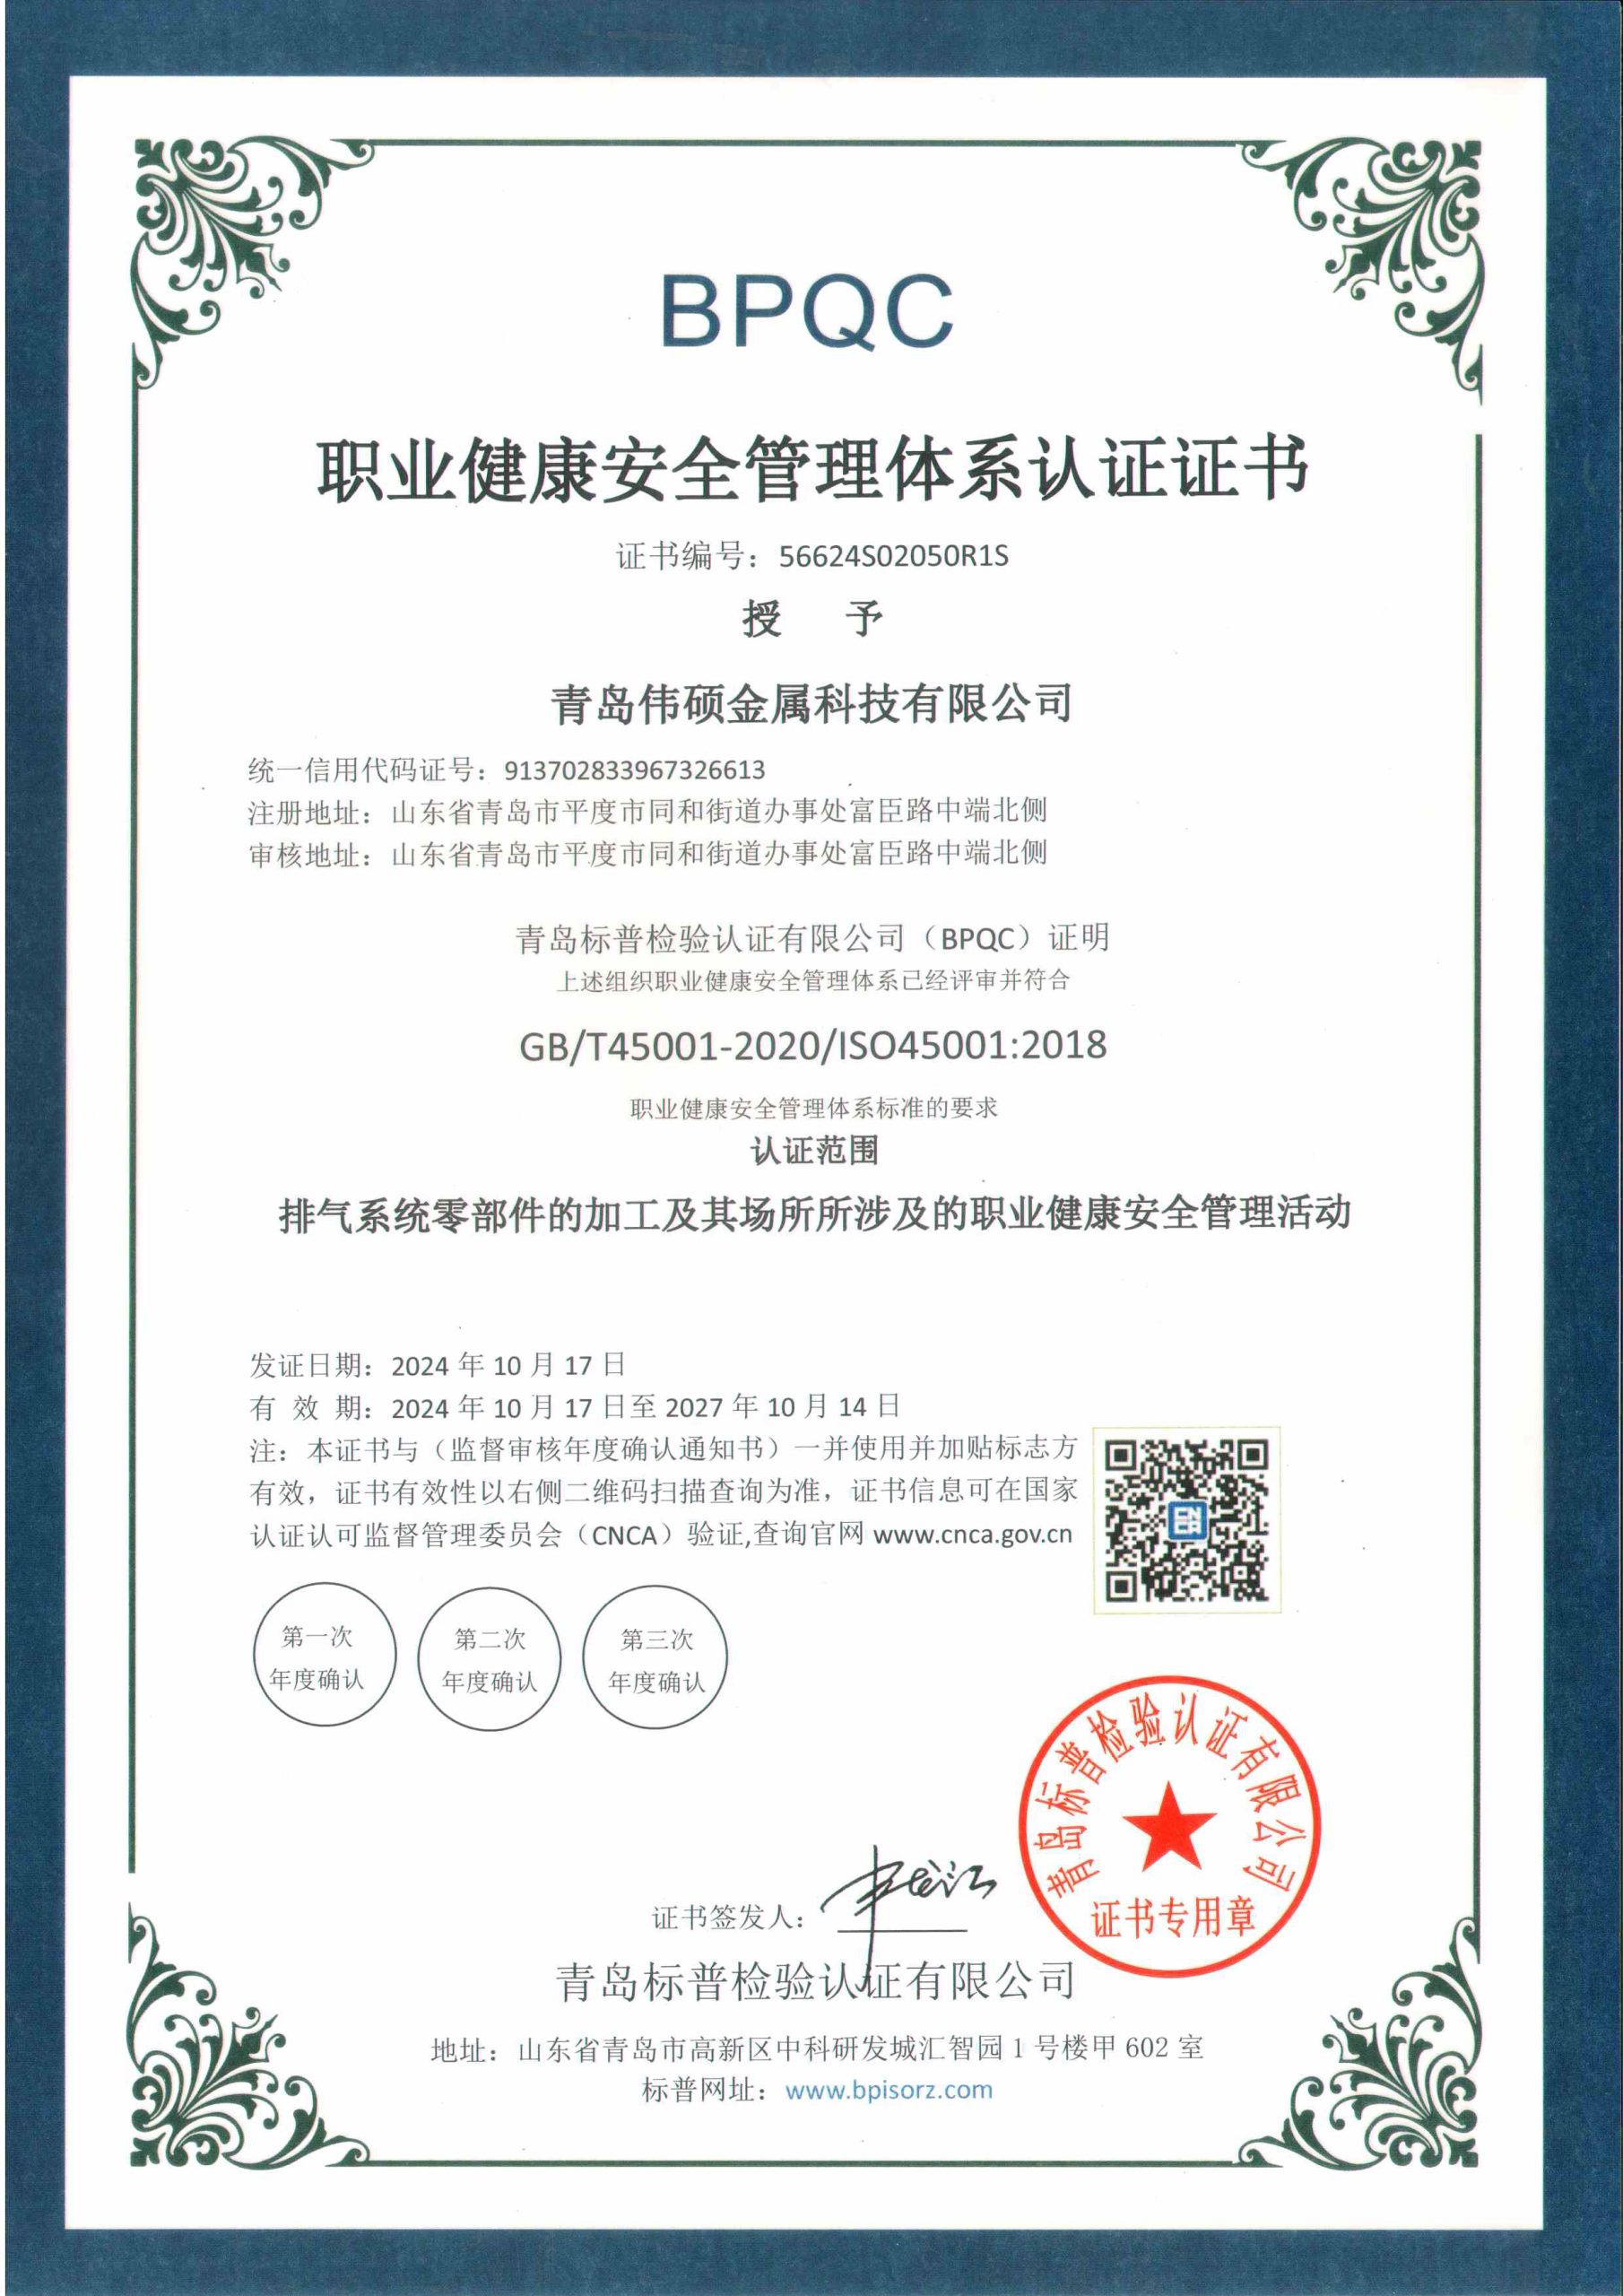
IATF 16949 quality management, environmental and occupational health & safety management certificates.
| The finished-part risk | Cast + machined at Waking | Foundry + separate machine shop |
|---|---|---|
| Porosity found after machining | X-ray screening before the cutter | Discovered at machined-part cost |
| Machining allowance | Set by the same engineers who design gating | Guessed from a drawing |
| Datum transfer | One datum plan, casting to final op | Argued between two vendors |
| Tolerance responsibility | One supplier owns the finished part | Each side blames the other |
| Paperwork | One traceable report set | Assembled from two companies |
One Quote, Three Steps
1. Send the Finished-Part Drawing
Material, quantity, machined surfaces marked, sealing and pressure requirements noted.
2. Combined Engineering Review
Castability, machining allowance and datum plan reviewed together — one quote for the finished part.
3. Cast, Machine, Inspect, Ship
X-ray before machining, CMM after, leak test where required, export packing with full reports.
Where Cast + Machined Parts Go
Flow Control
Powertrain & Housings
Machinery & Equipment
Valve Bodies Pump Housings Impellers Motor Housings Transmission Parts Machinery Components Flanged Fittings Custom Brackets
One Factory, Whole Responsibility
2002
Casting and machining together since
70,000 m²
Foundry + CNC floor, one site
400+
CNC machines finishing castings
40+
Export markets served
Frequently Asked Questions
Because the expensive failures happen in the handoff: porosity exposed by machining, allowances that don’t clean up, datums that don’t transfer. When both steps run in one plant, those risks are engineered out before production — and one supplier is responsible for the finished tolerance.
Structural and pressure-critical castings are screened on our XTH320 X-ray system before machining, so internal defects are caught at casting cost. Sealing faces that must be porosity-free are flagged on the inspection plan and verified after the finishing pass.
Cast surfaces keep casting tolerances; critical features are machined. Bores, seats, flange faces and threads are cut on our CNC floor and verified on COORD3 and ZEISS SPECTRUM coordinate measuring machines, with first article inspection before production.
Stainless steel 304, 316, CF8 and CF8M, carbon and alloy steel via investment casting, and aluminum alloy via low pressure and gravity casting — all machined in-house.
Yes. Pressure-containing parts such as valve bodies and housings go through leak testing as part of the production flow, after the sealing faces are machined.
Mark which surfaces are machined and which stay as-cast, flag sealing faces and porosity-sensitive zones, state the material grade and quantity. If anything is open, send the drawing anyway — the combined review will propose the plan.
Our machining is planned together with our own castings — that integration is the point. Send your drawing and requirements and we will confirm scope during the engineering review.
Tired of the Foundry-vs-Machine-Shop Blame Game?
Send the finished-part drawing once. Casting, machining, inspection and packing — quoted together, built together, answered for together.
Waking · Cast and machined components from one factory since 2002 · cnwakingcast@gmail.com · WhatsApp +86 150 0542 2253
