
Direct answer for lost wax casting design guide
Lost wax casting is strongest when a metal part needs complex geometry, repeatable detail, and less machining than a fully billet-machined route. The practical design question is not only whether the part can be cast, but which surfaces must remain as-cast, which surfaces need machining stock, and how the supplier will inspect those features after finishing.
Use this guide for stainless steel, alloy steel, or compact precision components where tooling, wax pattern control, shell quality, and machining allowance decide cost and repeatability. The commercial review should connect directly to lost wax casting service, CNC machining for cast components, casting quality inspection, send drawings and project requirements to Waking; those service pages are where a buyer can verify process capability, inspection scope, and RFQ next steps.
Design rules matter most when the foundry also machines the part. Waking works this way as an casting factory that machines its own parts, so wall thickness and datum decisions are reviewed against the machining plan.
Table of Contents
Buyer decision table
Many RFQs fail because drawings specify tight tolerances everywhere instead of separating cast features from machined datums and sealing faces. Use the table below as a quick screening tool before comparing quotations.
| Buyer checkpoint | Weak supplier response | Stronger Waking-style review |
|---|---|---|
| Wall and rib design | Part can be wax patterned but not filled consistently | Review thin sections, transitions, ribs, and local mass before tooling |
| Machined features | Tight dimensions are shown everywhere | Mark datums, sealing faces, bores, and threads that require machining |
| Material route | Grade is selected without casting review | Confirm castability, heat treatment, corrosion needs, and certificates |
| Sample approval | Only appearance is reviewed | Check dimensions, surface condition, machining stock, and functional surfaces |
Inspection and documentation evidence
Google’s helpful-content guidance rewards pages that give visitors enough useful detail to complete their task. For casting buyers, useful detail means the page should help them prepare a cleaner RFQ, ask sharper supplier questions, and reduce rework during samples. The evidence below is practical rather than decorative.
| Evidence to request | Why it matters | When to ask |
|---|---|---|
| Process recommendation | Shows whether the supplier understood geometry, alloy, and volume | Before tooling quotation |
| Machining plan | Prevents datum and stock problems after casting | Before sample build |
| Inspection record | Turns quality claims into reviewable evidence | During sample and batch approval |
| Document package | Avoids export and customer acceptance delays | Before shipment |
RFQ checklist before asking for price
- Current 2D drawing with revision, units, tolerances, material, finish, and critical dimensions.
- 3D model in a usable format, plus notes about any surfaces that must not be changed.
- Target annual quantity, first order quantity, sample quantity, and expected production rhythm.
- Application environment, assembly function, load, sealing, corrosion, or temperature notes where relevant.
- Required documents such as material certificate, dimensional report, test record, or buyer inspection form.
- For lost wax casting, mark machined stock, thin walls, deep cavities, and areas where surface detail matters.
Common mistakes to avoid
- Comparing suppliers only by unit price while ignoring tooling assumptions, machining scope, inspection records, and packaging requirements.
- Sending a drawing without identifying critical-to-function dimensions, sealing faces, assembly surfaces, or any areas that must be protected during finishing.
- Expecting a casting supplier to guess the correct material standard, surface finish, or documentation package without written RFQ notes.
- Approving samples visually without checking whether later production batches will be inspected the same way.
For a project-specific review, use lost wax casting service, CNC machining for cast components, casting quality inspection, send drawings and project requirements to Waking. While preparing the drawing, RFQ and inspection notes, compare this requirement with custom metal casting manufacturer guide, low pressure aluminum casting capability, gravity casting and low pressure process review, CNC machining after casting. Ask Waking to review lost wax casting feasibility together with CNC machining stock and inspection points before tooling release.
FAQ
What should a buyer prepare before contacting Waking?
Prepare a current drawing, 3D model, material requirement, quantity estimate, critical dimensions, surface finish notes, and any inspection or document requirements. If a requirement is uncertain, mark it as open instead of leaving it implied.
Should every tolerance on a casting drawing be tight?
No. Tight tolerances should be reserved for functional features. Many cast surfaces can use a practical casting tolerance, while bores, threads, sealing faces, and assembly datums may need CNC machining and inspection.
How should a buyer compare two casting quotations?
Compare process route, tooling assumptions, sample scope, machining work, inspection records, packaging, lead time, and exclusions. A lower unit price can be misleading if it excludes work that the project still needs.
Sources and benchmark references
Lost wax casting is useful when stainless steel or alloy steel parts need complex geometry, tighter detail and less machining than a rougher casting route. The best results come when design, tooling, gating, machining and inspection are considered together.
This guide is written for purchasing teams, engineers and quality teams who need production-ready metal components rather than a vague supplier introduction. It connects the commercial question to process choice, drawing review, machining, inspection and documentation.
Quick Answer
For process design, start with the application and the drawing. Then check whether the casting process, material, machining plan and inspection method support the final part requirement. A low quote is only useful when the scope is clear enough to compare.
On the Waking site, related commercial pages include lost wax casting, CNC machining, quality system. Those pages explain the production routes; this article explains how to make the buying or engineering decision.
Decision Table
| Decision point | What to check |
|---|---|
| Geometry | Good for complex shapes, ribs, bosses and internal details that are hard to machine from billet. |
| Material | Often used for stainless steel, carbon steel and alloy steel components. |
| Machining stock | Critical surfaces still need controlled machining allowance. |
| Inspection | Use first article checks before moving into repeat production. |
How to Review the Requirement
Begin with the function of the component. A bracket, housing, valve part, pump component or automotive part may look simple in a photo, but the real requirement is usually hidden in mating surfaces, loads, threads, sealing faces and inspection notes.
Separate the part into three zones: cast surfaces, machined surfaces and controlled functional features. Cast surfaces need process stability. Machined surfaces need datum control and enough stock. Functional features need inspection rules that both buyer and supplier understand.
Common Buyer Mistakes
- Sending a 3D file without a 2D drawing, material grade or tolerance notes.
- Comparing quotes that include different machining, finishing or inspection scope.
- Waiting until after tooling to discuss draft, wall thickness or machining datums.
- Specifying tight tolerances on surfaces that do not affect function.
- Ignoring packaging, corrosion protection and documentation until shipment.
Practical Checklist
- Geometry: Good for complex shapes, ribs, bosses and internal details that are hard to machine from billet.
- Material: Often used for stainless steel, carbon steel and alloy steel components.
- Machining stock: Critical surfaces still need controlled machining allowance.
- Inspection: Use first article checks before moving into repeat production.
What to Ask a Supplier
Ask how the supplier reviews drawings before tooling. Ask which dimensions are expected to be cast, which will be machined, and which need first article inspection. Ask what information is missing from the RFQ before asking for the lowest price.
For technical references, buyers often align drawings and inspection language with sources such as ISO 9001 quality management, ASTM standards, ASME Y14.5 GD&T and NIST measurement resources. Use the standard required by your project; do not assume a supplier will know it unless it appears on the drawing or purchase document.
Where to go next
Continue with low pressure aluminum casting capability. For context from the previous topic, review Custom Metal Casting Manufacturer Guide for Production Buyers. If you are building the full supplier selection workflow, return to the custom metal casting manufacturer guide.
When the drawing is ready, you can send drawings and project requirements to Waking for review.
FAQ
Is lost wax casting the same as investment casting?
In many buyer conversations the terms are used together, although suppliers may define process details differently.
Does lost wax casting remove all machining?
No. It can reduce machining, but tight fits, threads, bearing seats and sealing surfaces usually still need machining.
What makes a drawing ready for lost wax casting?
Clear material, tolerance zones, datum scheme, surface finish and inspection notes make the review much faster.
If the casting route is still open, compare this investment casting design path with low pressure aluminum casting design limits and gravity versus low pressure casting tradeoffs before committing tooling assumptions.
Frequently Asked Questions
Which surfaces should be left as-cast versus machined on a lost wax stainless steel part?
Use as-cast surfaces where the investment casting tolerance and surface finish are acceptable, and reserve CNC machining for functional features such as bores, threads, sealing faces, and assembly datums. Waking reviews thin sections, ribs, and local mass before tooling and machines its own castings, so datum and machining stock decisions can be checked against the machining plan.
What inspection evidence should I expect for a lost wax stainless steel component?
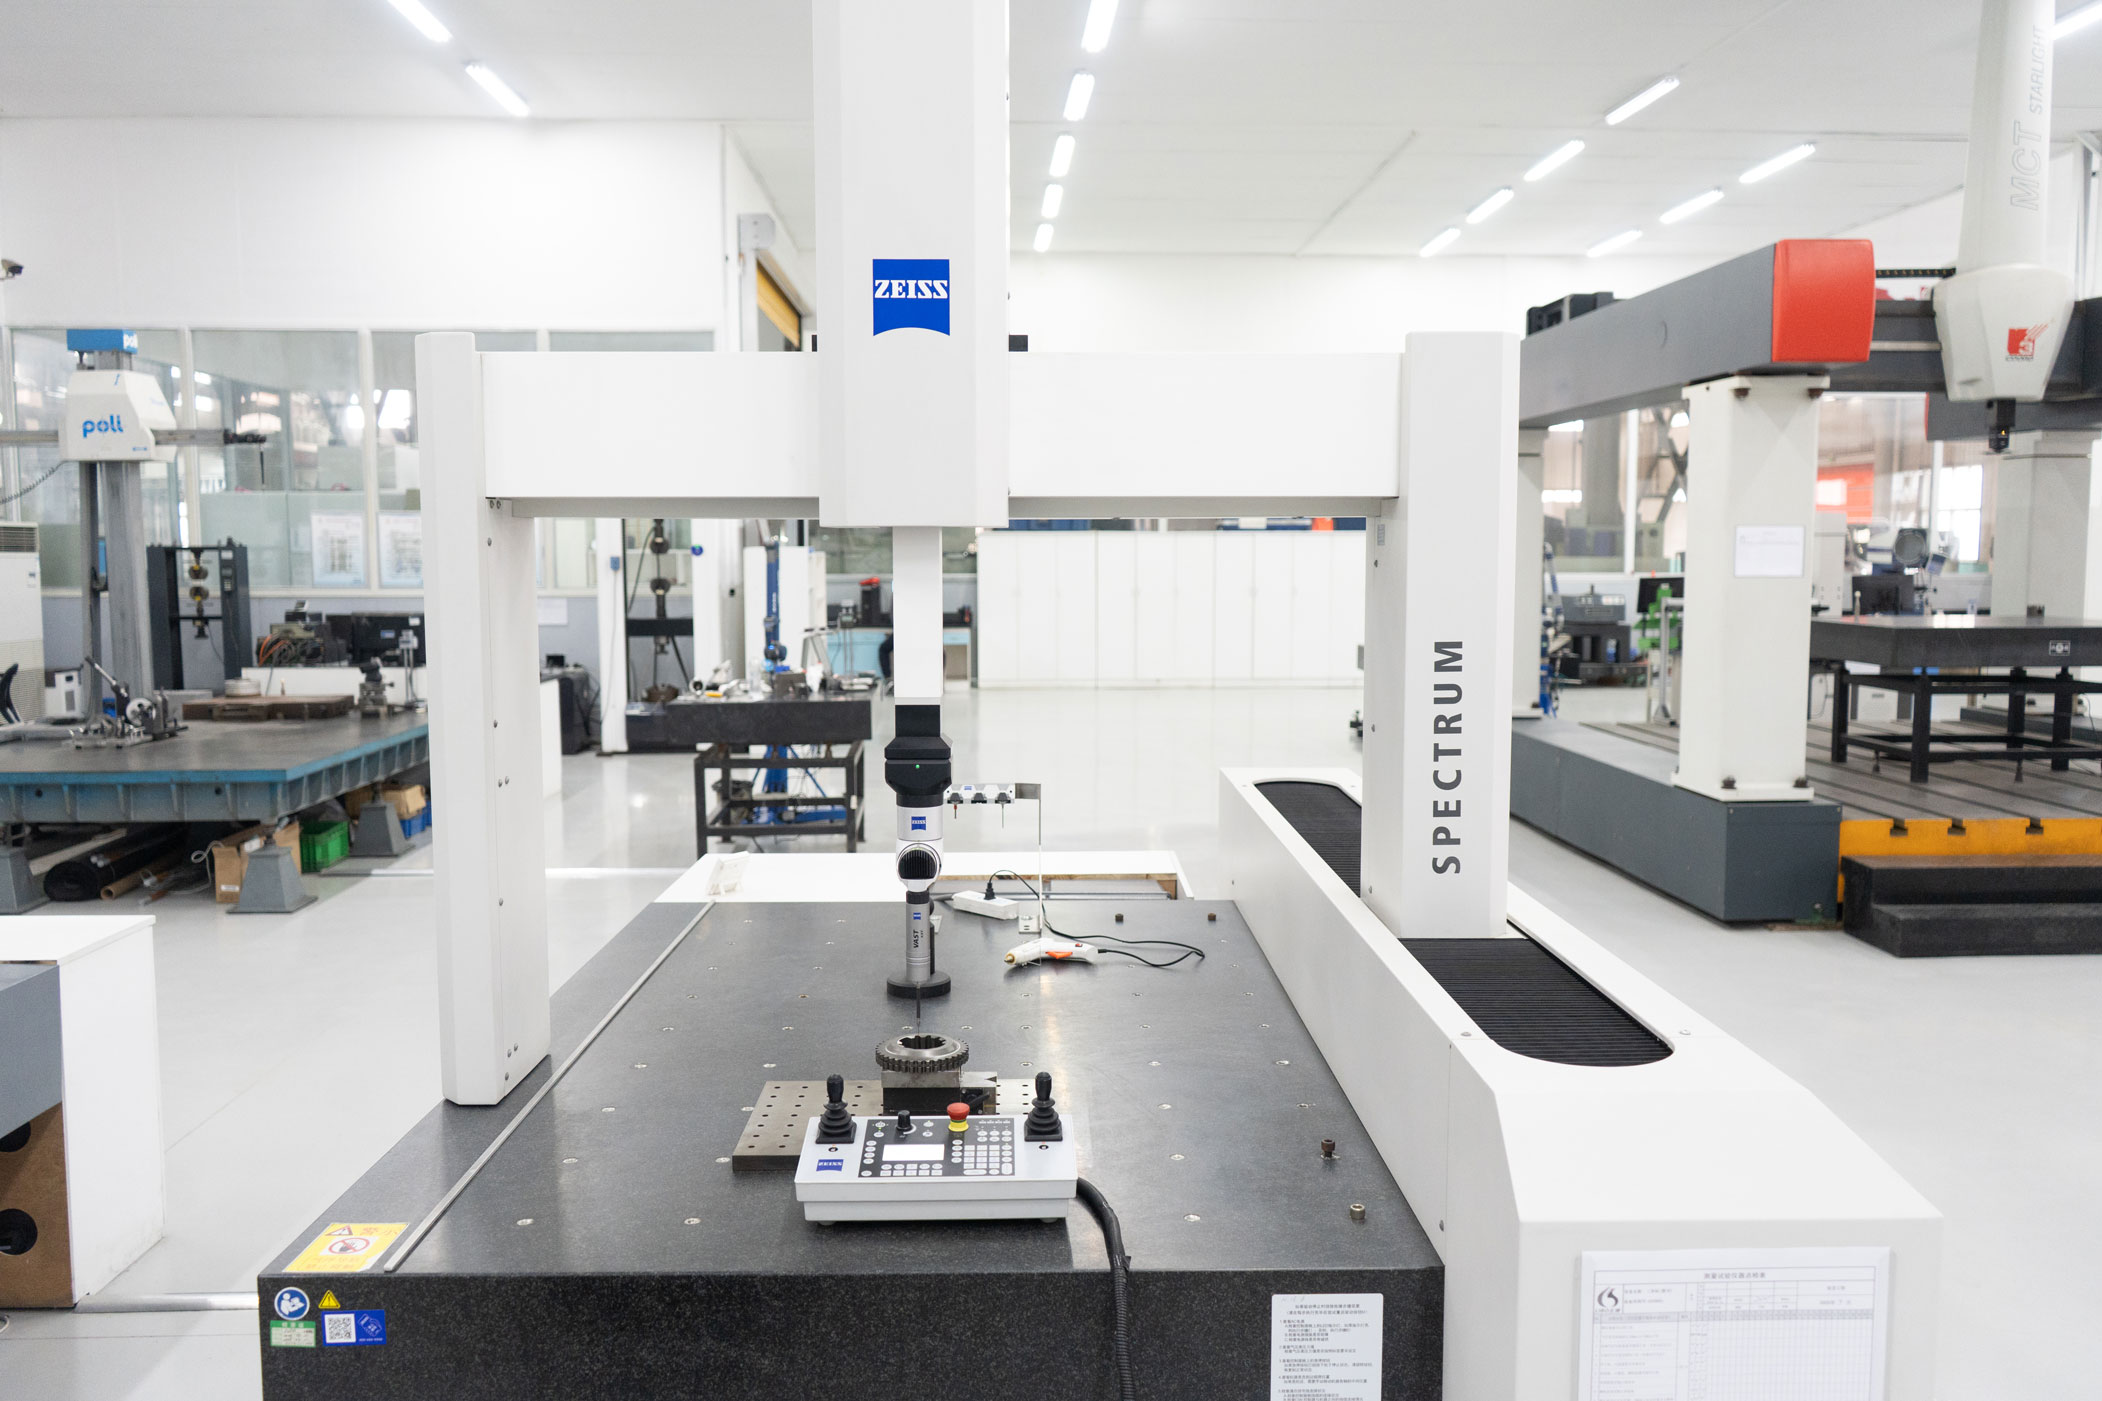
Request dimensional reports, surface condition checks, machining stock verification, and functional surface review. Waking can provide CMM inspection using COORD3 and ZEISS SPECTRUM machines, X-ray nondestructive testing with XTH320, hardness testing, roundness and profile measurement, first article inspection, sample approval, and batch traceability with material certificates. Avoid visual-only sample approval.
How should wall thickness and rib design be reviewed before tooling?
Work with the foundry to review thin sections, transitions, ribs, and local mass before tooling release. For Waking, this review is linked to CNC machining after casting, so wall and datum decisions are checked against how the part will be held and machined.
Can Waking cast stainless steel grades such as 304, 316, CF8, and CF8M and handle required post-processing?
Yes, Waking's silica sol lost wax casting covers stainless steel 304, 316, CF8, and CF8M, as well as carbon steel and alloy steel. In-house post-treatment includes deburring, cleaning, polishing, passivation, plating, coating, and heat treatment; specific requirements should be stated in the RFQ.
Key Parameters at a Glance
| Checkpoint | What to verify | Waking capability / reference |
|---|---|---|
| Wall and rib design | Review thin sections, transitions, ribs, and local mass before tooling release. | Casting and CNC review done in the same factory |
| As-cast vs machined features | Mark datums, sealing faces, bores, and threads for CNC machining; reserve tight tolerances for functional features. | Waking machines its own castings to the drawing datums |
| Material route | Confirm castability, heat treatment, corrosion needs, and certificates. | Stainless steel 304/316/CF8/CF8M, carbon steel, alloy steel |
| Inspection evidence | Check dimensions, surface condition, machining stock, and functional surfaces. | CMM (COORD3, ZEISS SPECTRUM), X-ray (XTH320), hardness, roundness/profile, FAI, sample approval, leak testing, batch traceability and material certificates |
| Post-treatment | Specify required finish and protection. | Deburring, cleaning, polishing, anodizing, plating, passivation, coating, heat treatment |
